Explore our elite tier of heavy-duty industrial racks, retail display hardware, and smart supermarket logistics gear designed for maximum durability.
Driving global commercial infrastructure with precision engineering, massive industrial capacity, and unwavering quality compliance.
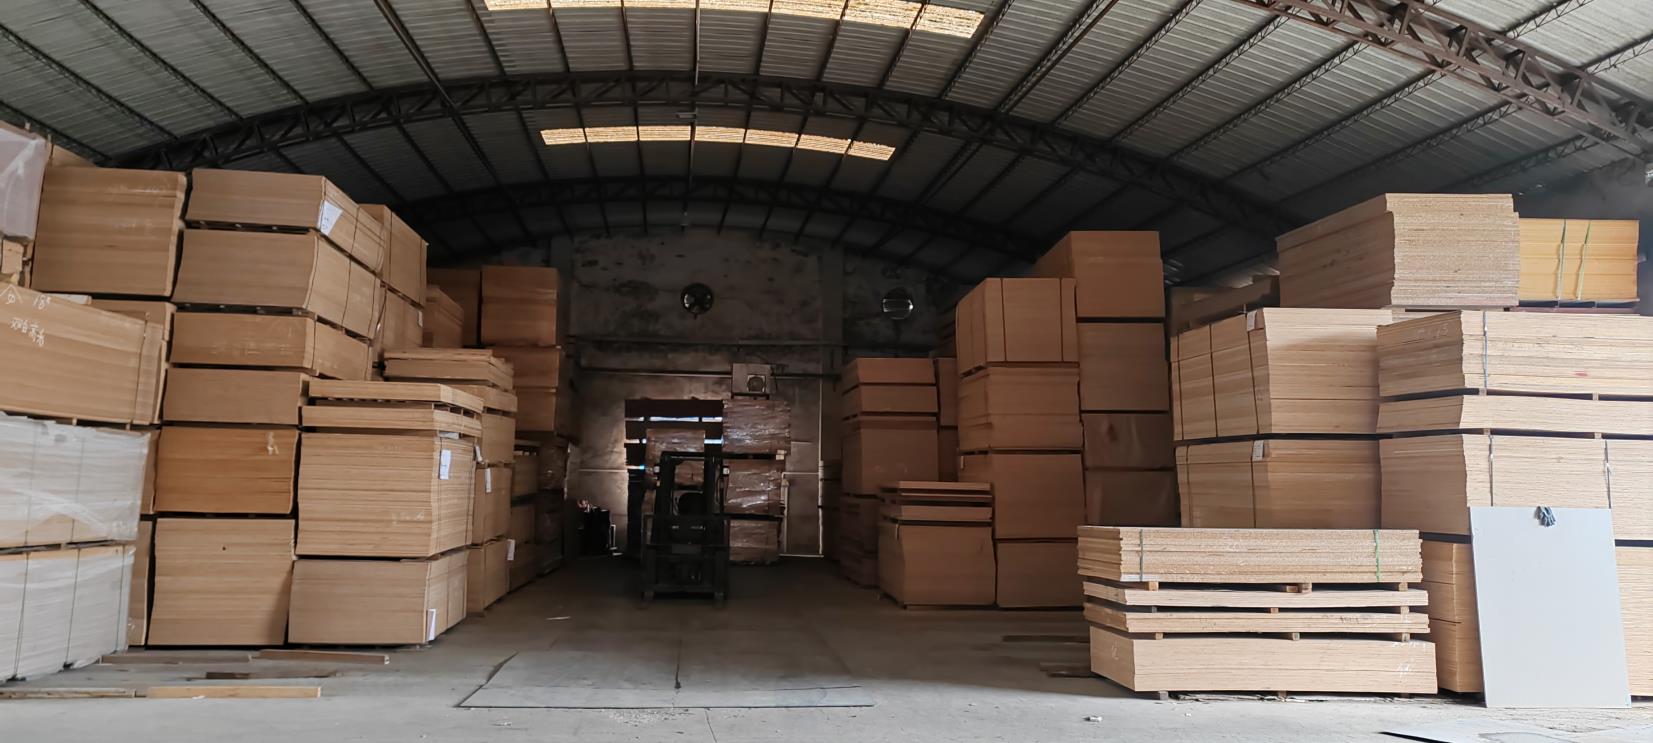
Established in 2016, Nanjing Fortis Storage Equipment Manufacturing Co., Ltd. commands a modern industrial plant covering 48,000 m². Driven by 10 years of deep industry expertise and 7 years of global trade experience, our annual export turnover reaches $35 million. We uphold strict quality control through ISO14001 and TUV standards, performing automated CMM dimensional inspections and salt spray corrosion testing with 62 full-time QA personnel.
As a direct factory exporter, our key commercial footprints span Western Europe, South America, and the Middle East, integrated with a network of over 1,400 supply chain partners. Our client base mainly includes mega-warehouse developers, cold chain storage operators, and global retail chains. Our robust R&D team of 80 engineers specializes in bespoke structural adaptations, special surface coating treatments, and high-density racking configurations, introducing 350 innovative products to the global market last year.
Navigating the complexities of modern warehousing, automated fulfillment, and omni-channel retail architecture worldwide.
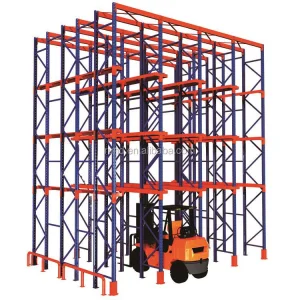
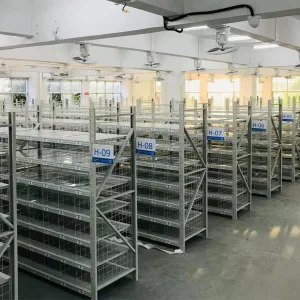
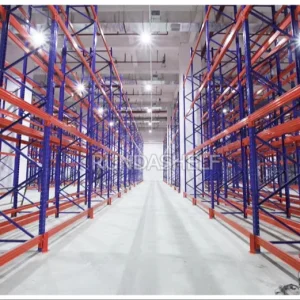
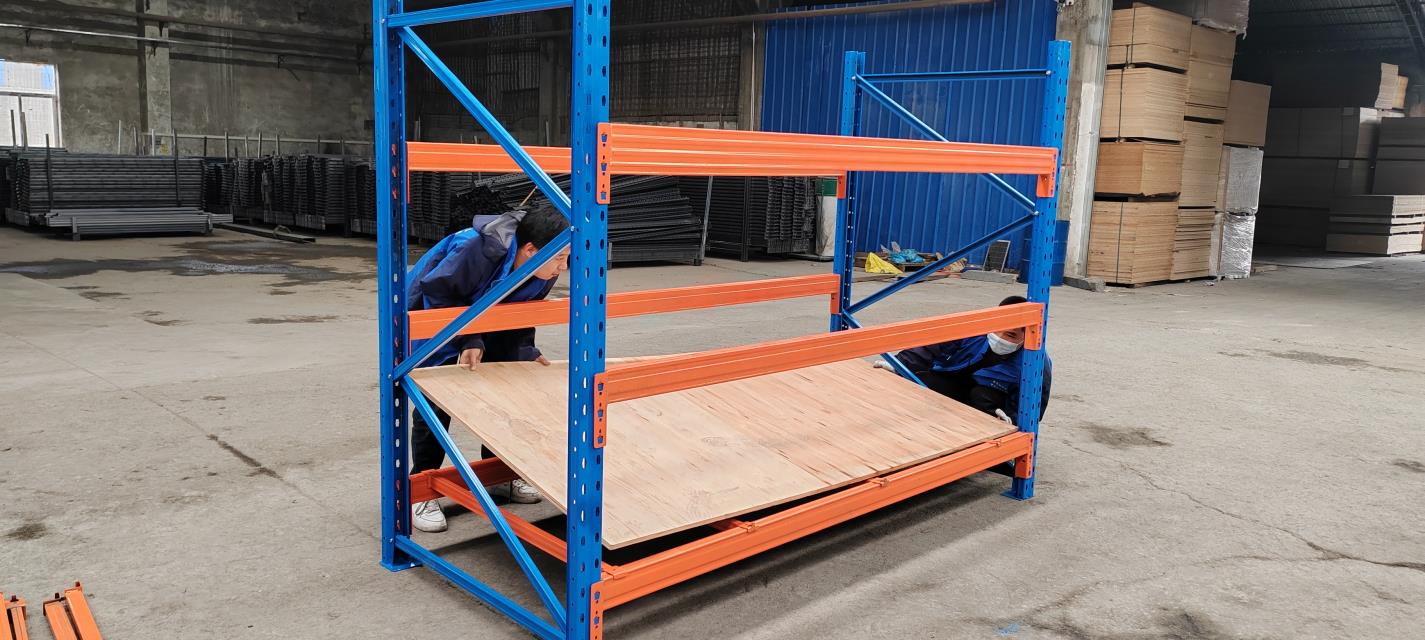
With the exponential growth of e-commerce, modern fulfillment centers require maximum vertical storage capacity. Our heavy-duty pallet racks and boltless shelving units engineered with advanced structural steel optimization empower logistics giants to reduce footprint overheads while accelerating automated inventory retrieval workflows.
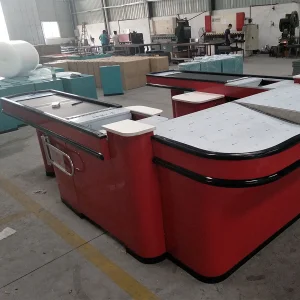
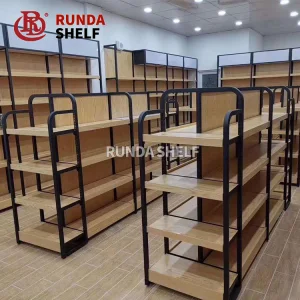
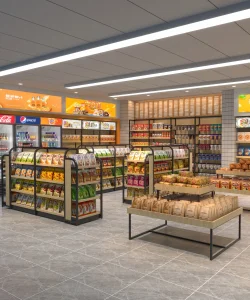
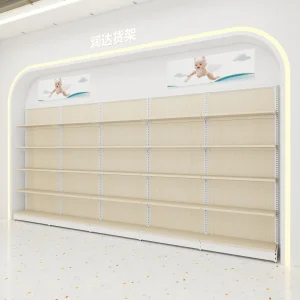
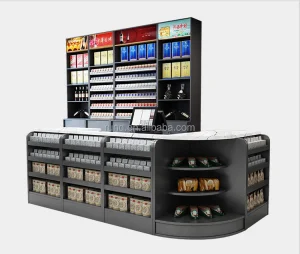
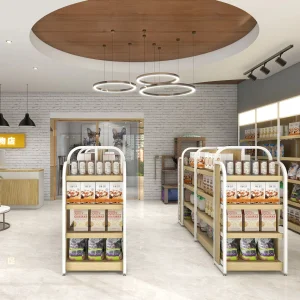
The contemporary retail landscape demands sensory-rich, aesthetically optimized merchandising layouts. Our hybrid steel-wood gondola shelves and cashier counters blend structural rigidity with luxury architectural finishings, enhancing consumer dwell time and elevating brand prestige across global supermarket chains.
Operating under extreme thermal and mechanical stresses requires specialized anti-corrosion coatings and load-bearing verification. Our products undergo rigorous TUV-certified salt spray testing to guarantee uncompromised structural integrity in refrigerated and hazardous industrial environments.
Ensuring seamless international deployment through stringent international certifications and bespoke engineering adjustments.
Compliance is the cornerstone of global trade. We maintain strict adherence to ISO14001 environmental management frameworks and TUV safety standards. Every production batch undergoes automated Coordinate Measuring Machine (CMM) dimensional analysis managed by our dedicated team of 62 quality assurance inspectors.
Market requirements vary significantly between Western Europe, Latin America, and the Middle East. Our 80-strong engineering division provides rapid-response localization services, adjusting load parameters, seismic coefficients, and aesthetic finishes to match regional building codes and retail consumer habits perfectly.
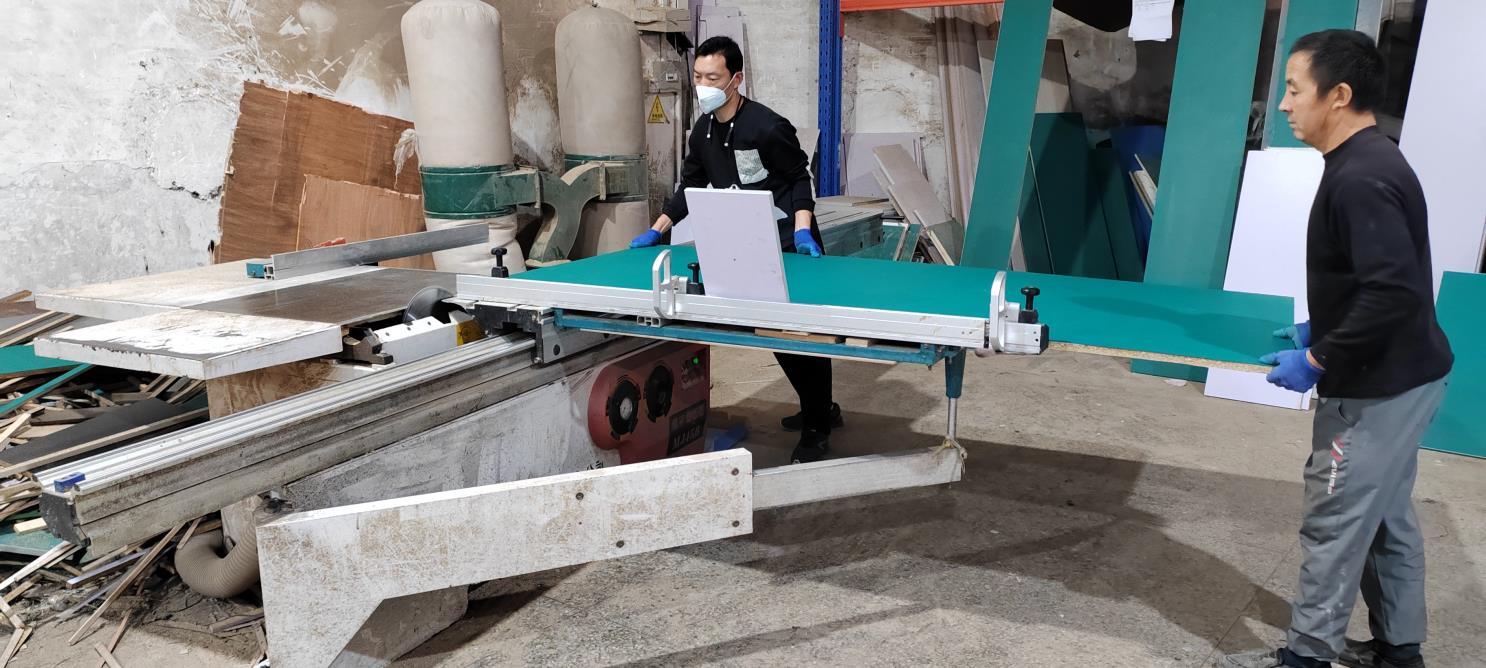
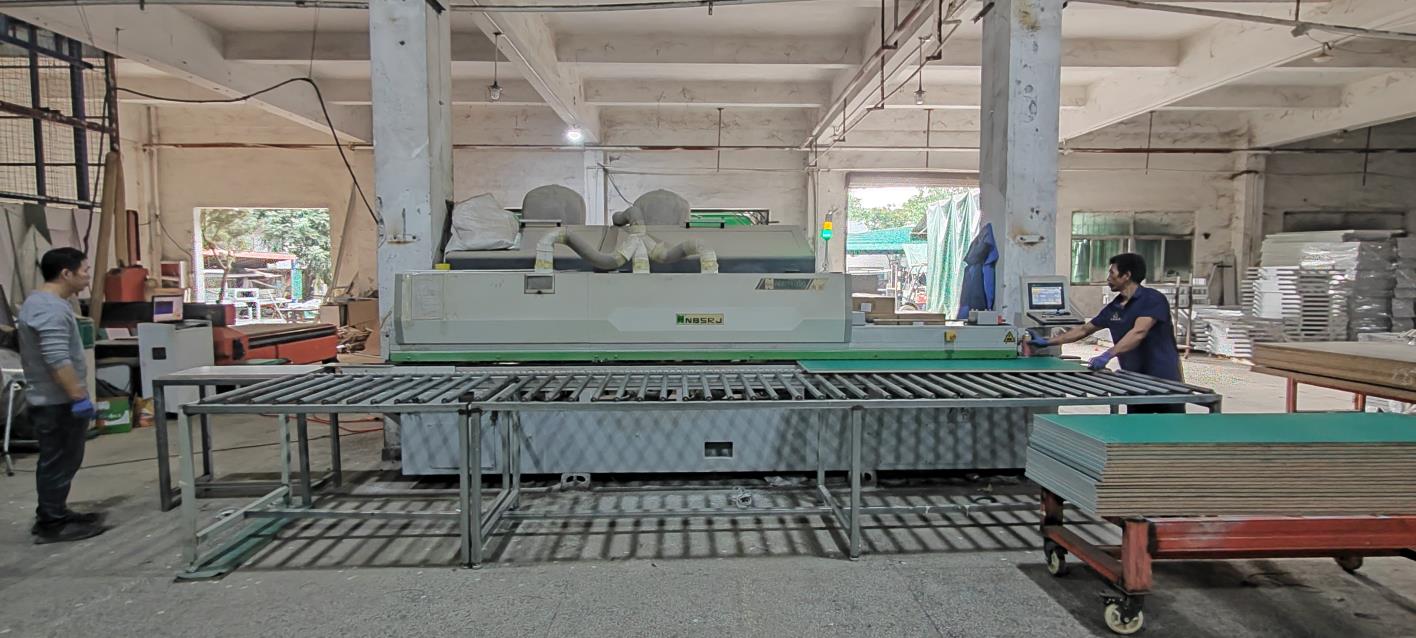
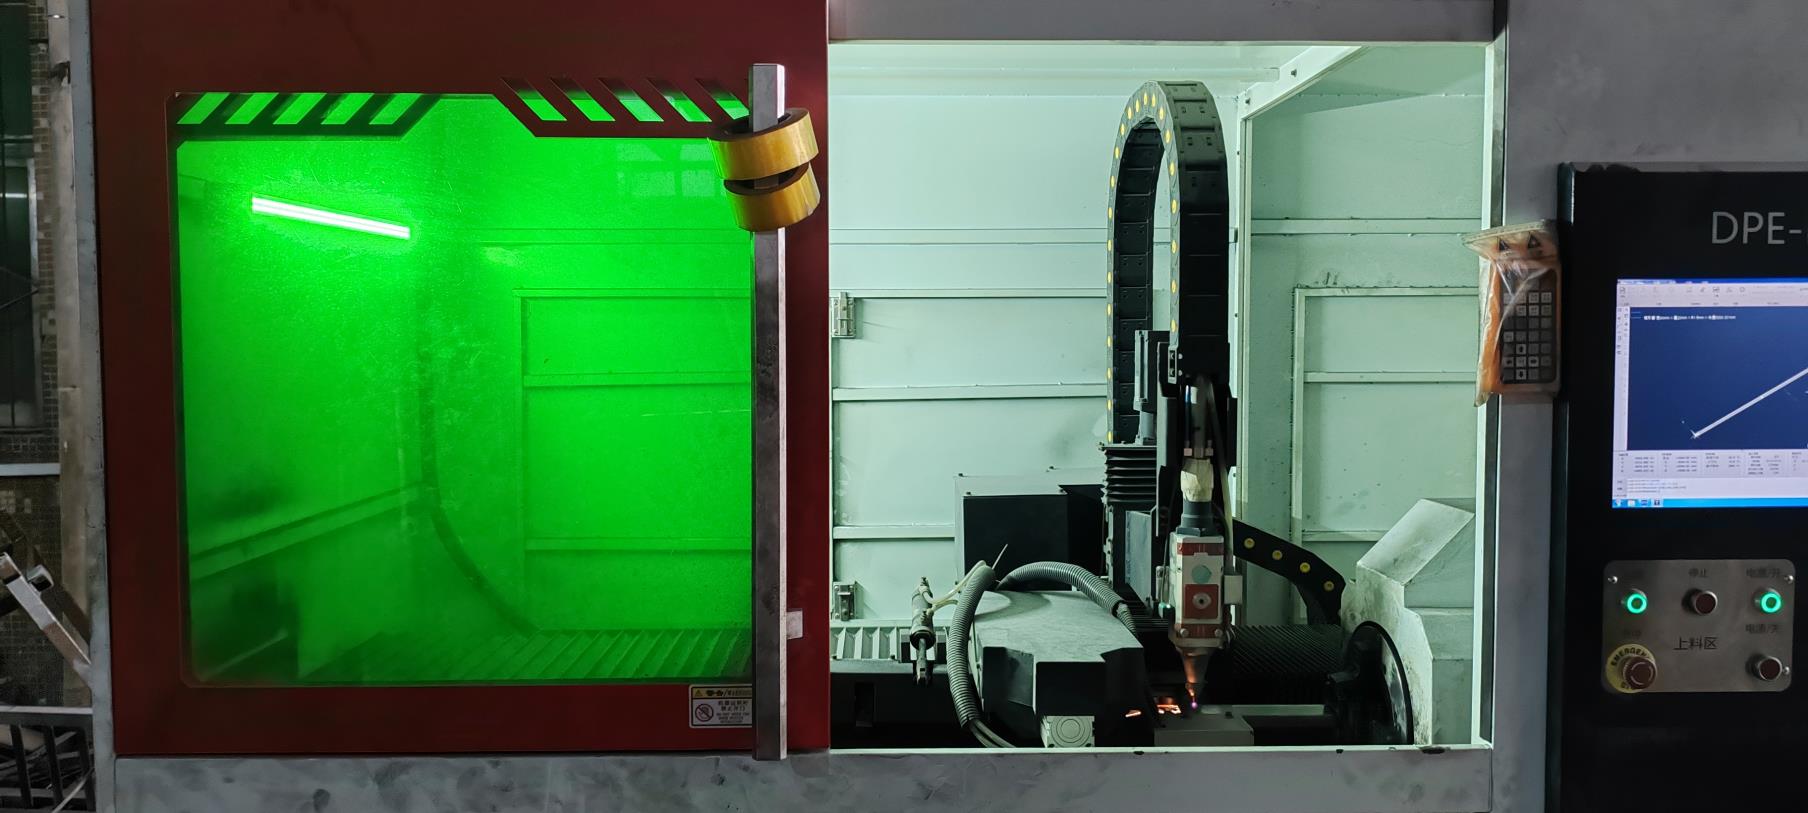
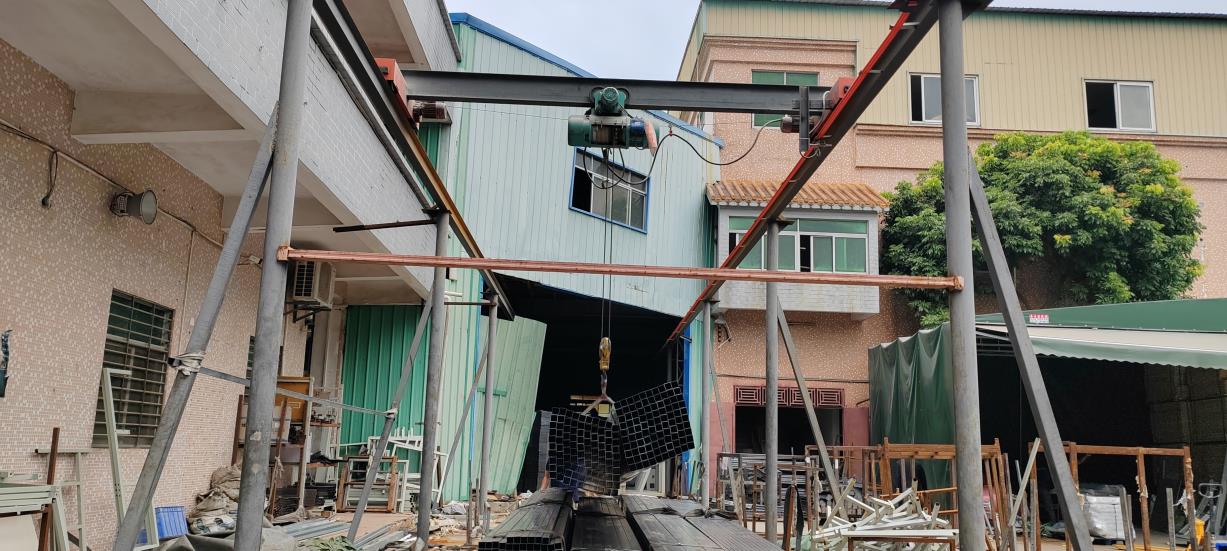
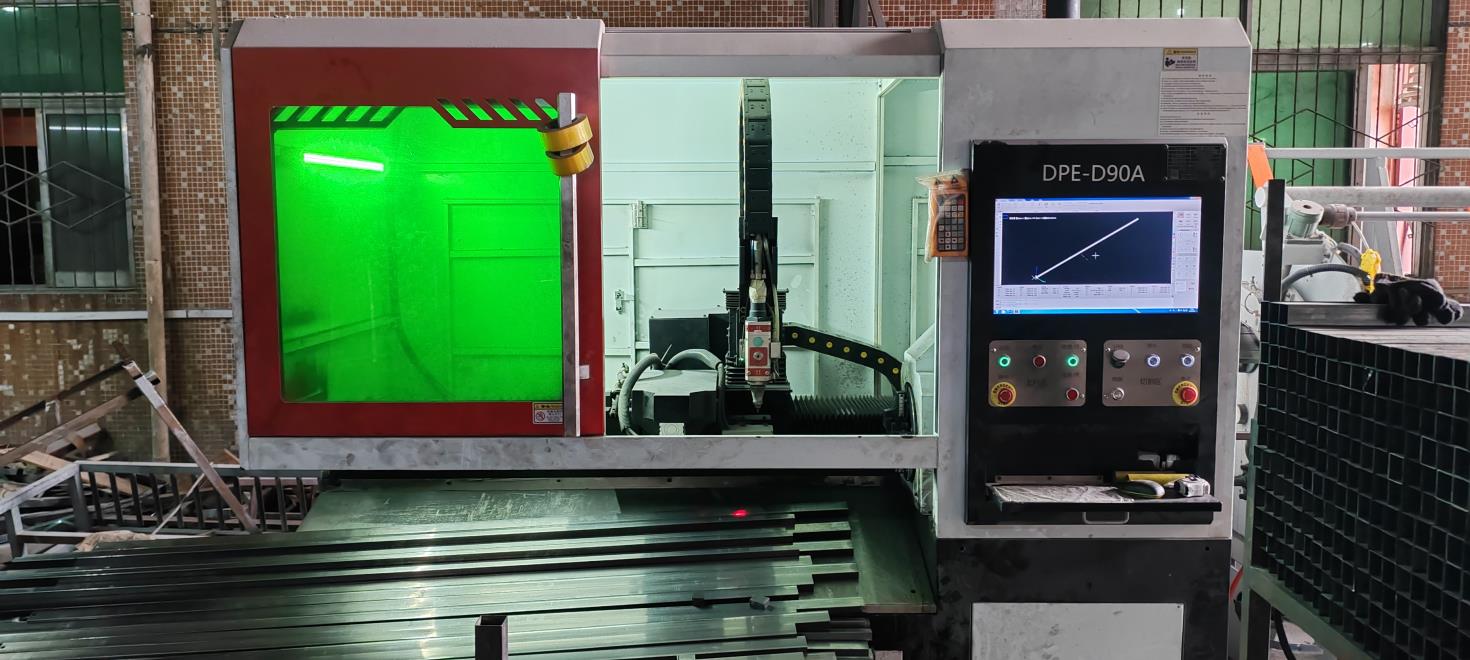
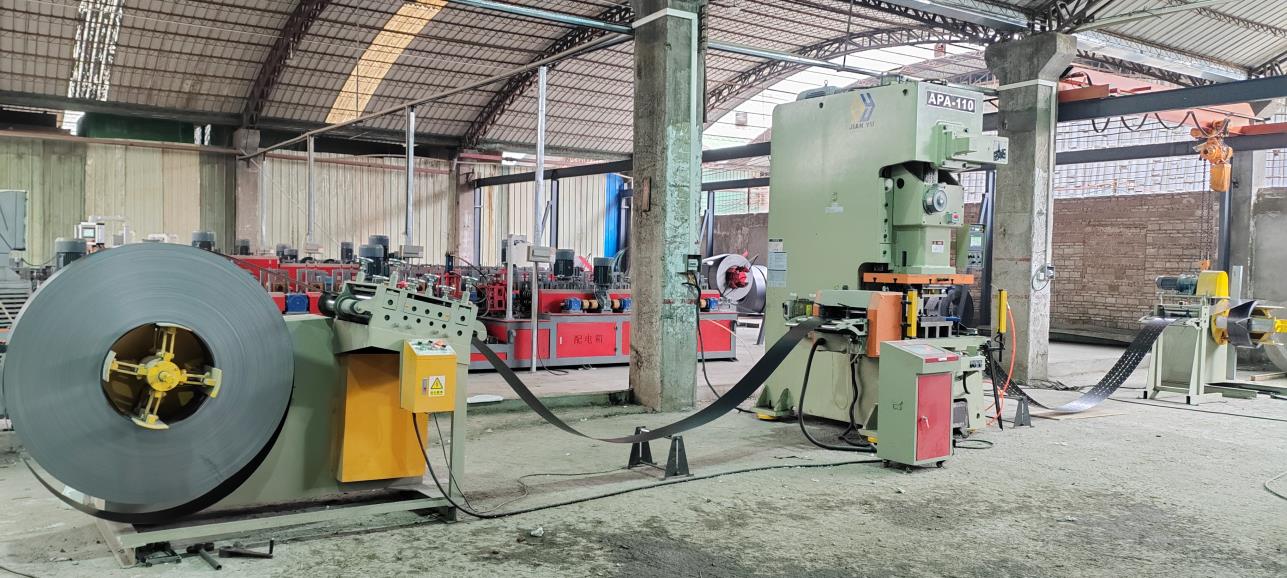
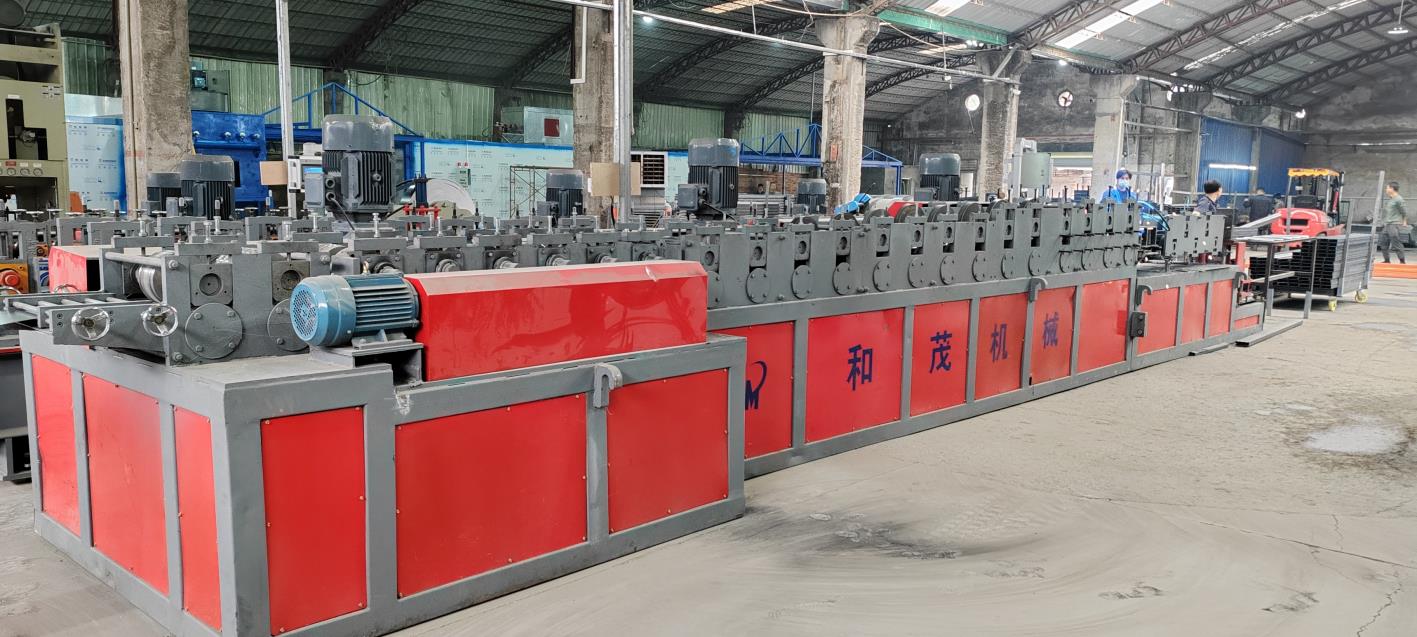
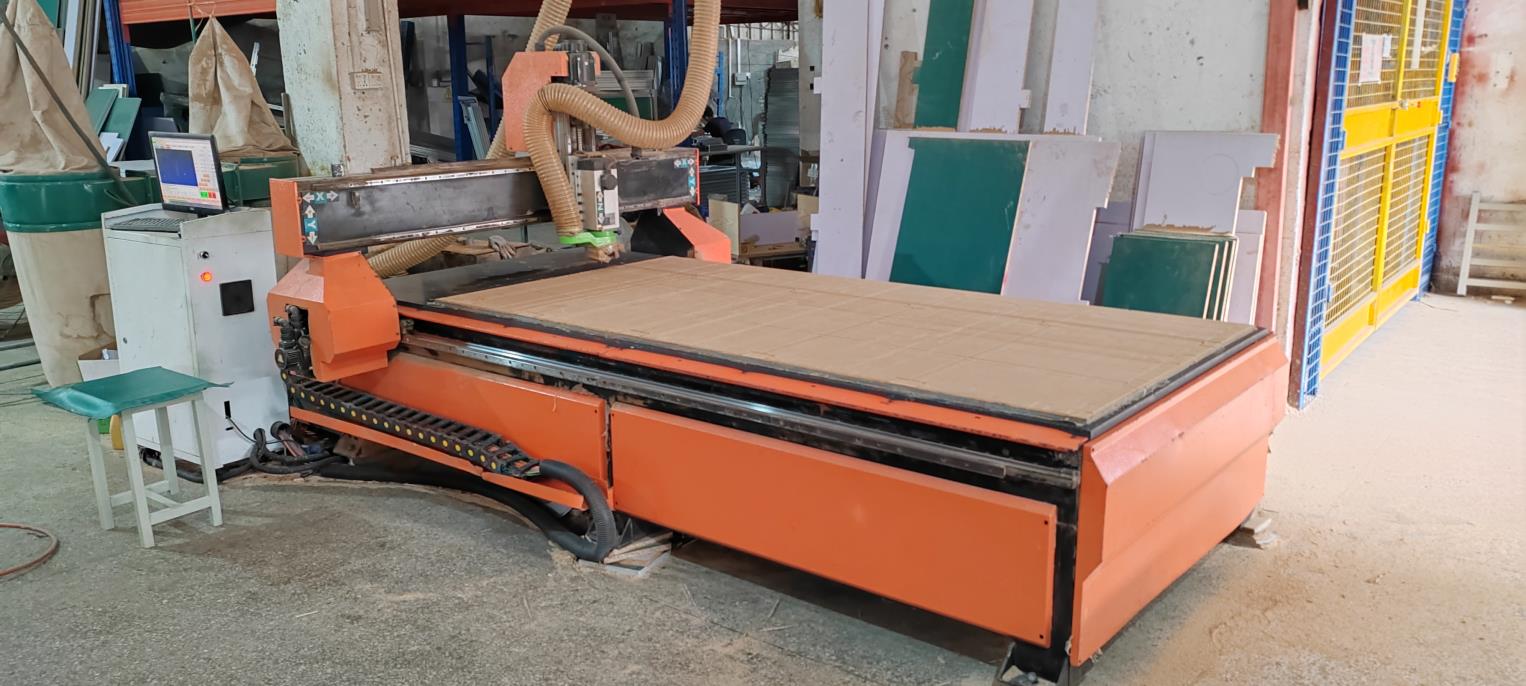
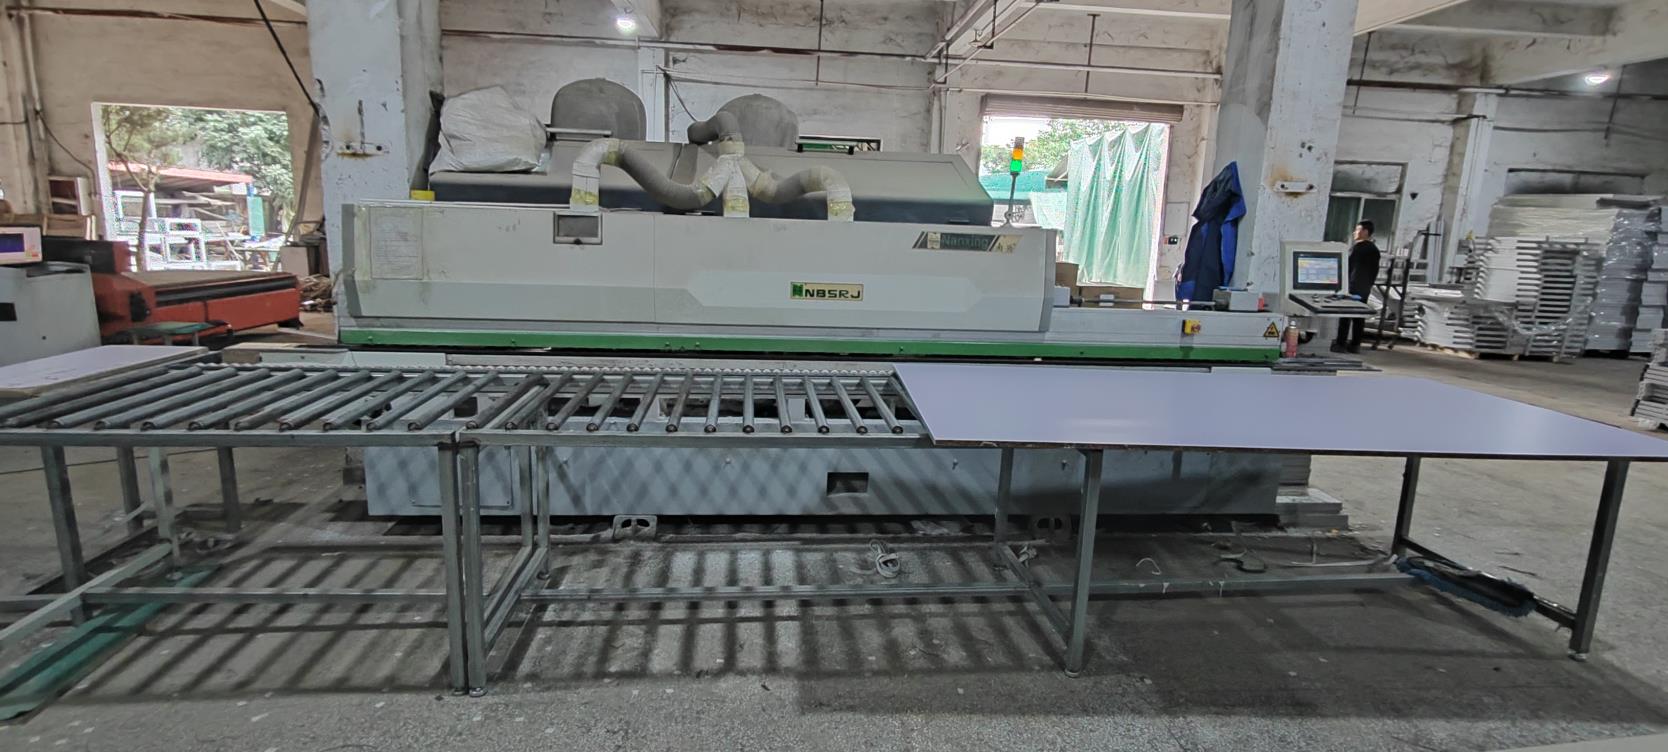
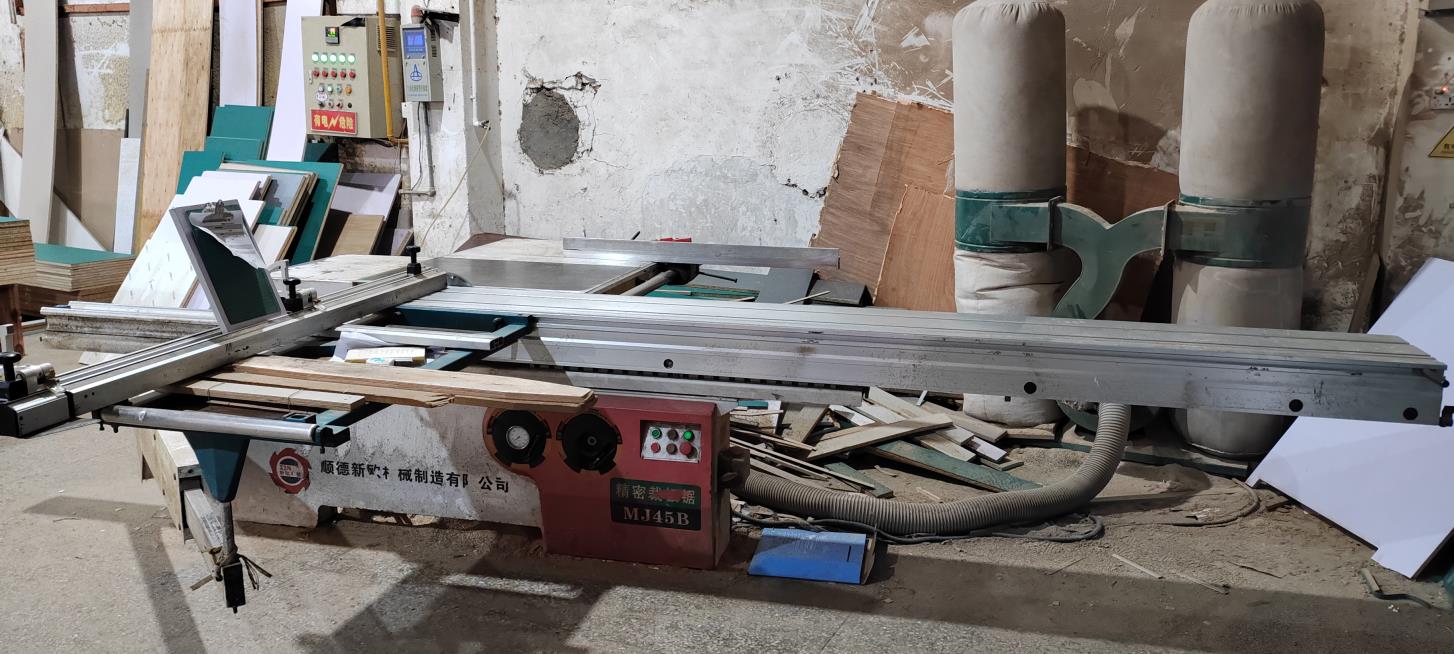
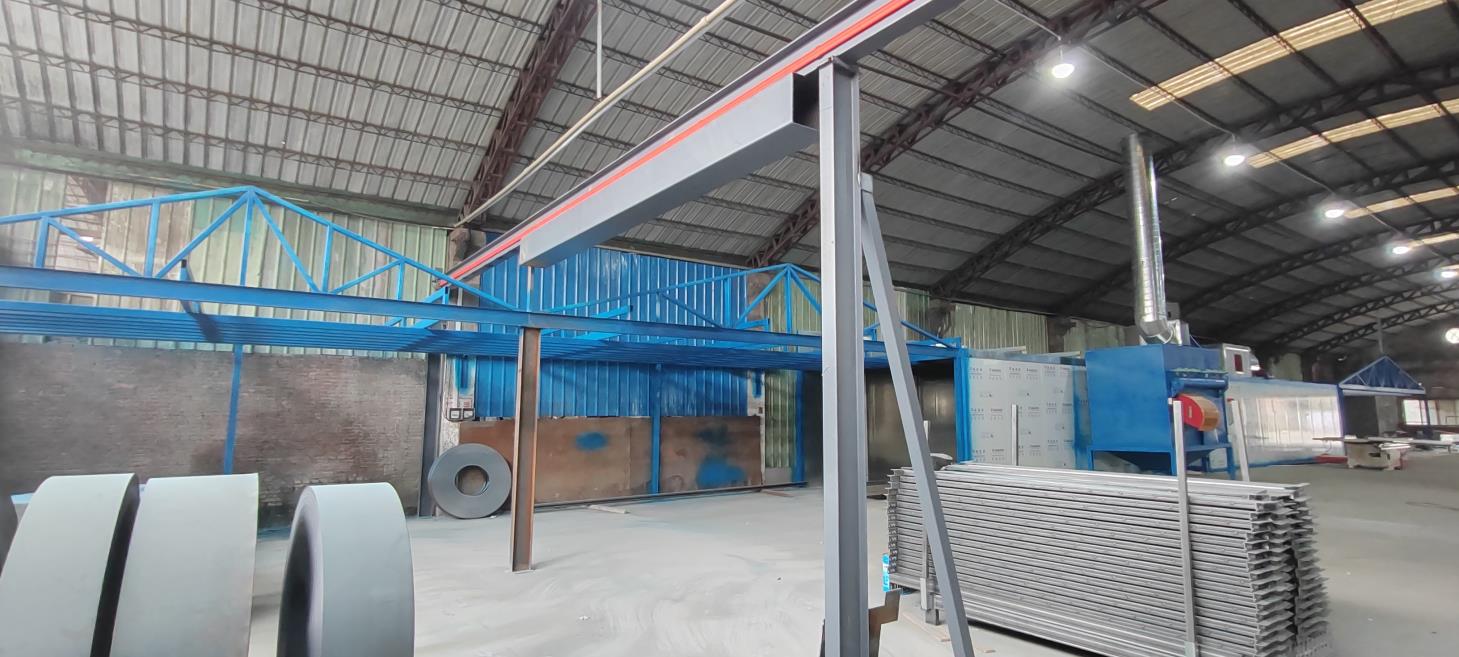
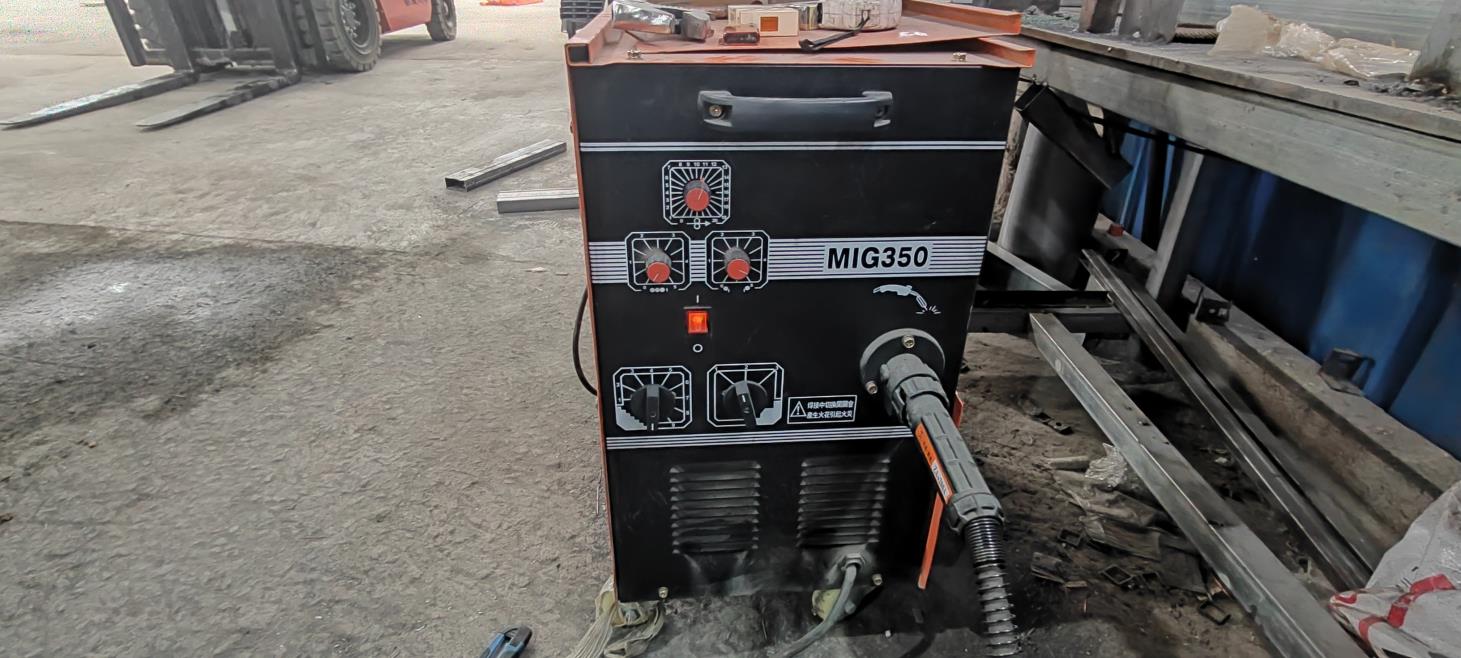
A transparent look at our advanced manufacturing workflow, transforming raw steel and wood into world-class commercial shelving systems.
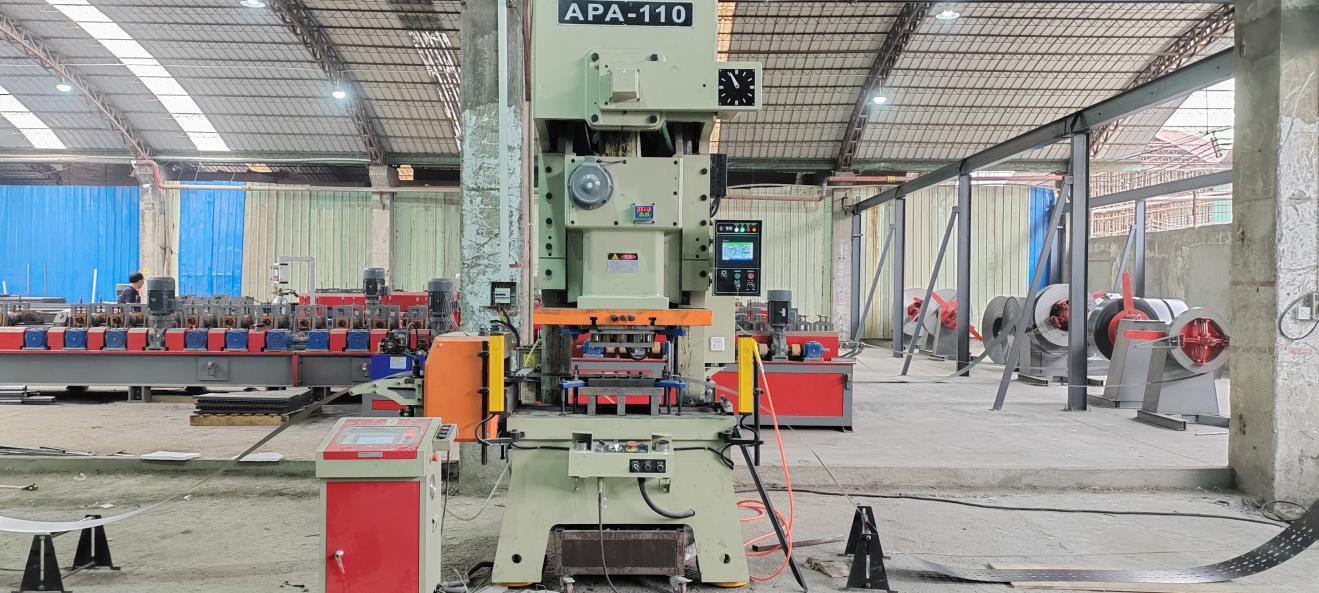
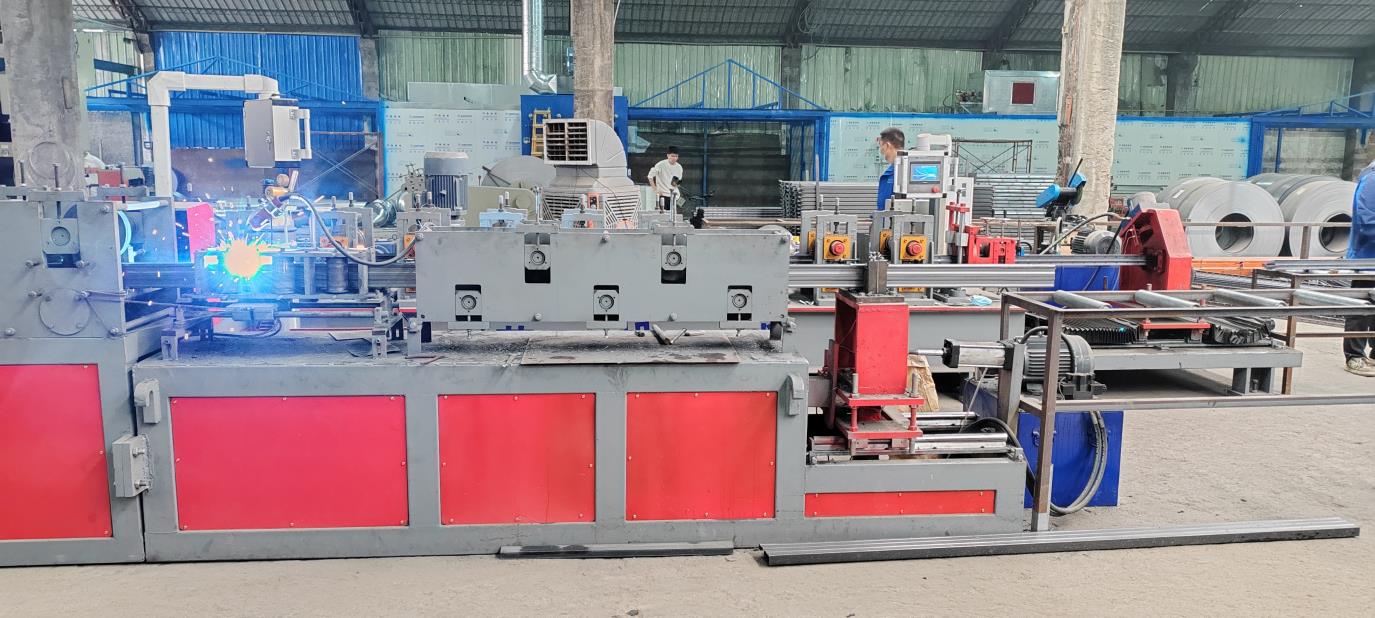
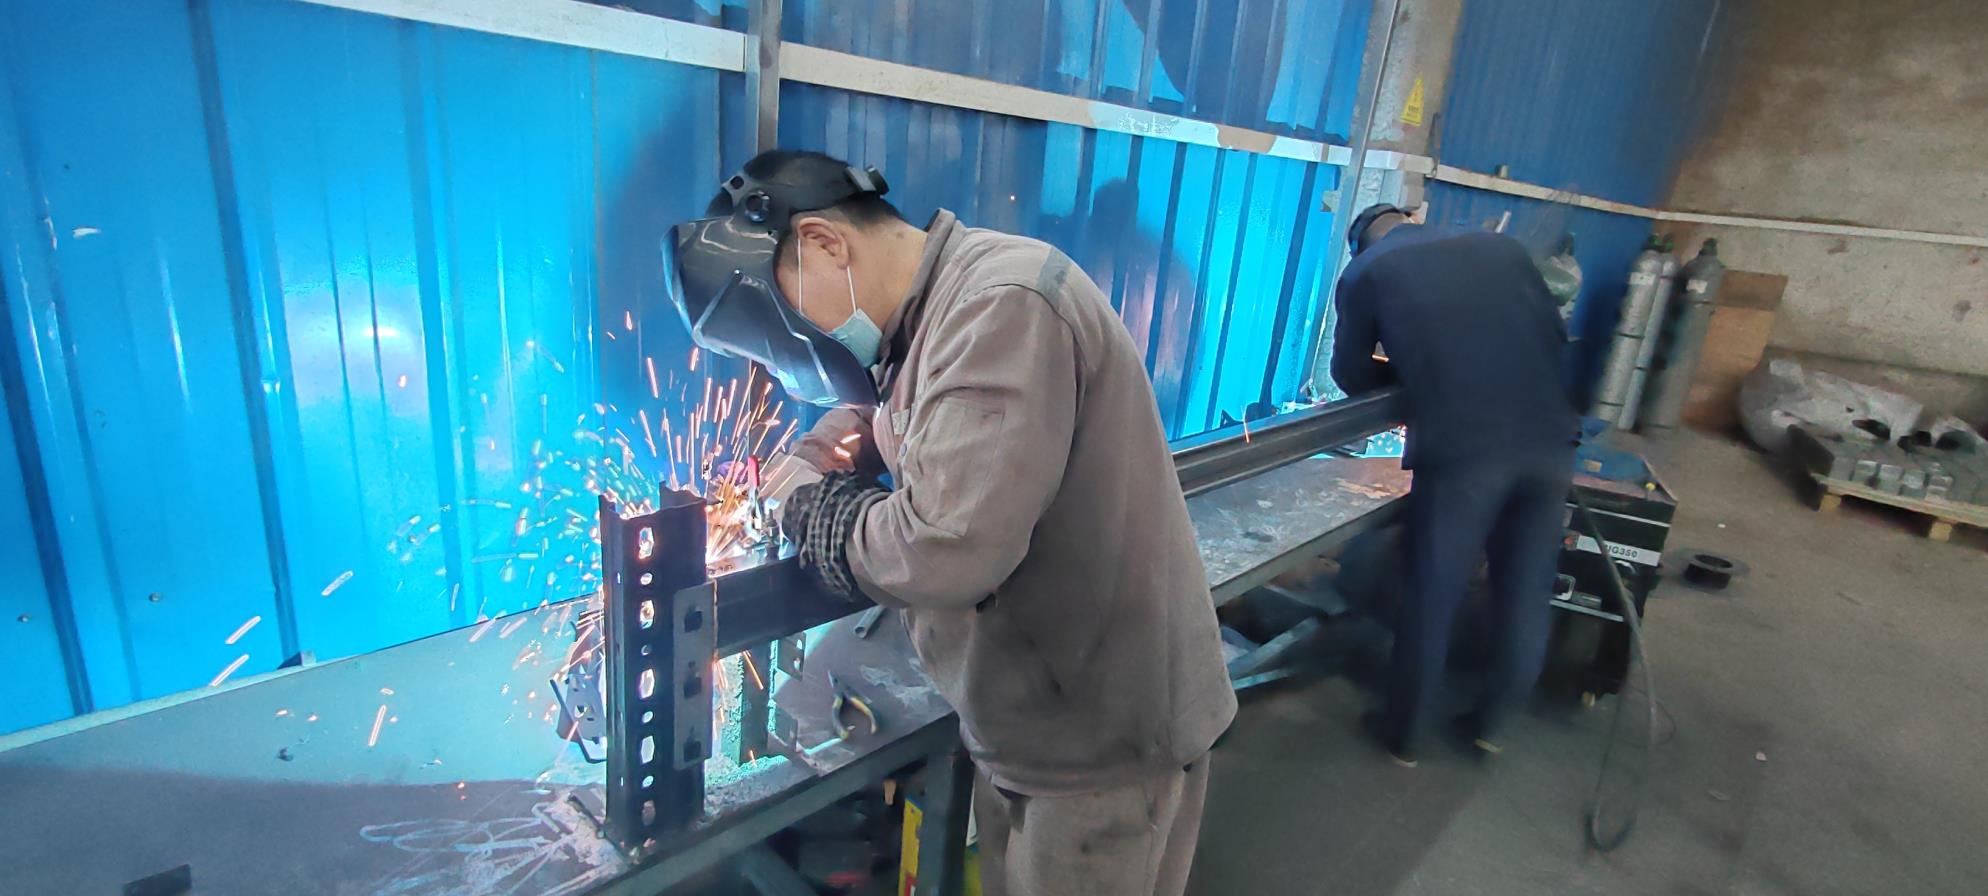
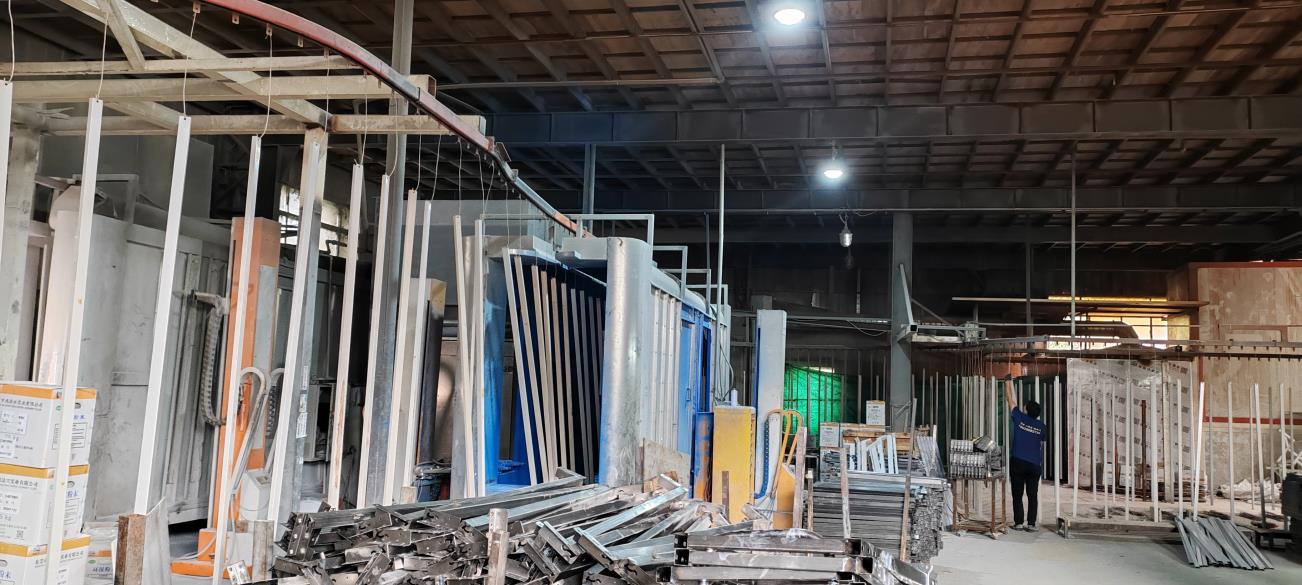
Pioneering the next generation of smart warehousing and intelligent retail architecture through continuous R&D investment.
Integrating weight sensors and RFID tracking directly into commercial shelving frames to provide real-time inventory visibility and automated restocking triggers for modern warehouses and automated retail setups.
Transitioning toward carbon-neutral steel processing and eco-friendly powder coating formulations that minimize environmental impact while increasing structural longevity under harsh operating conditions.
Deploying advanced design software backed by our 80-person engineering team to instantly configure bespoke modular racking systems tailored precisely to complex architectural floor plans.
Expert answers to critical technical and commercial inquiries regarding our global commercial shelving solutions.
Our manufacturing operations strictly adhere to ISO14001 environmental management standards and TUV product safety certifications. Each structural unit undergoes rigorous CMM dimensional checks and automated salt spray corrosion testing to ensure absolute reliability in global markets.
Yes. With a dedicated R&D team of 80 senior engineers and a 48,000 m² production facility equipped with advanced laser cutting and automated stamping machines, we specialize in tailoring structural dimensions, weight capacities, and surface finishes to precise client specifications.
We manage an annual export turnover exceeding $35 million, supplying major warehouse developers and retail chains across Western Europe, South America, and the Middle East with highly optimized supply chain logistics and reliable lead times.
Discover our extended lineup of specialized display stands, shopping trolleys, grocery racks, and heavy-duty storage infrastructure.
 FortisRack