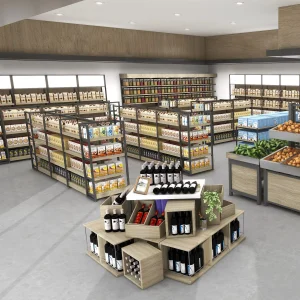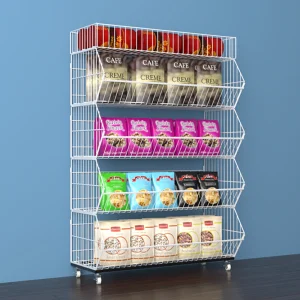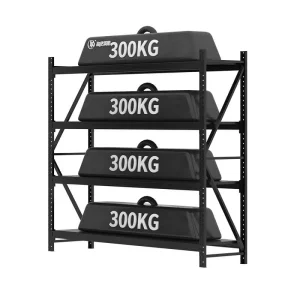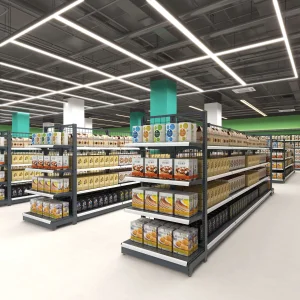
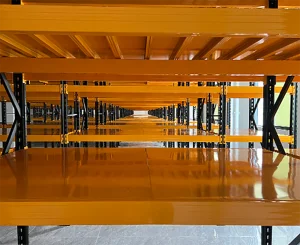
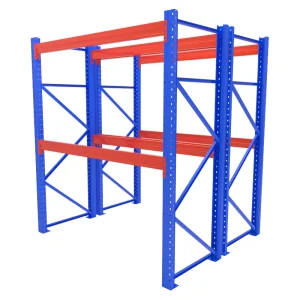
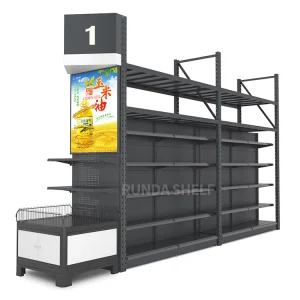
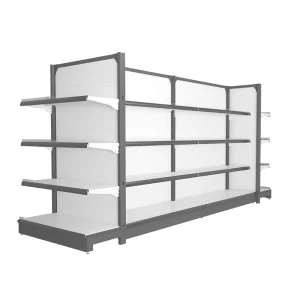
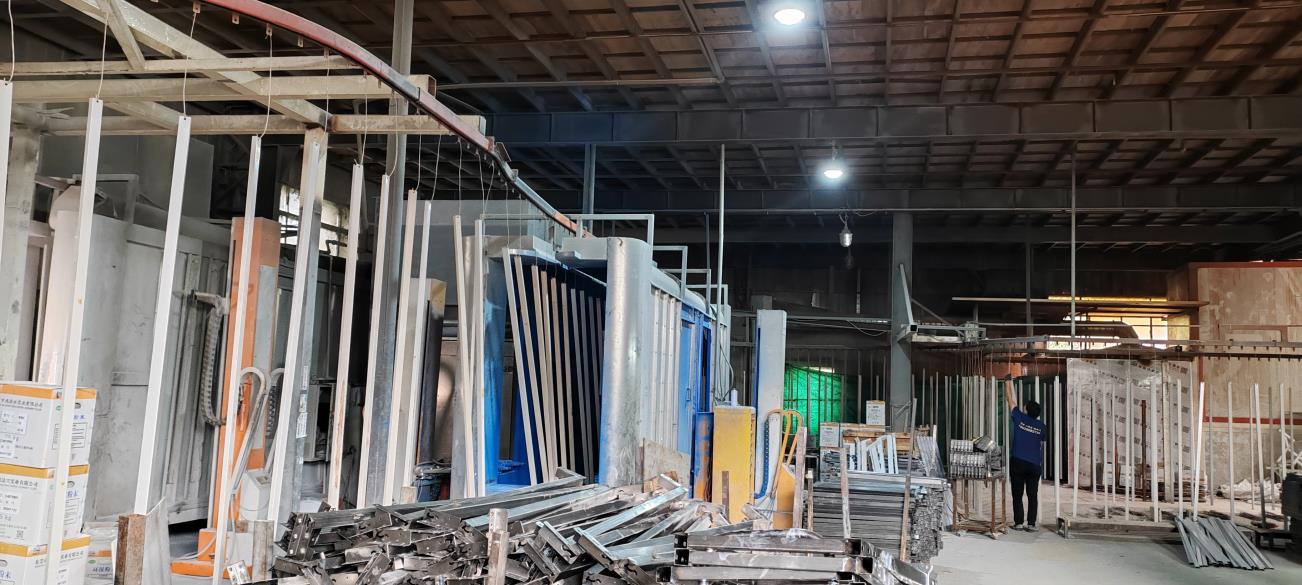
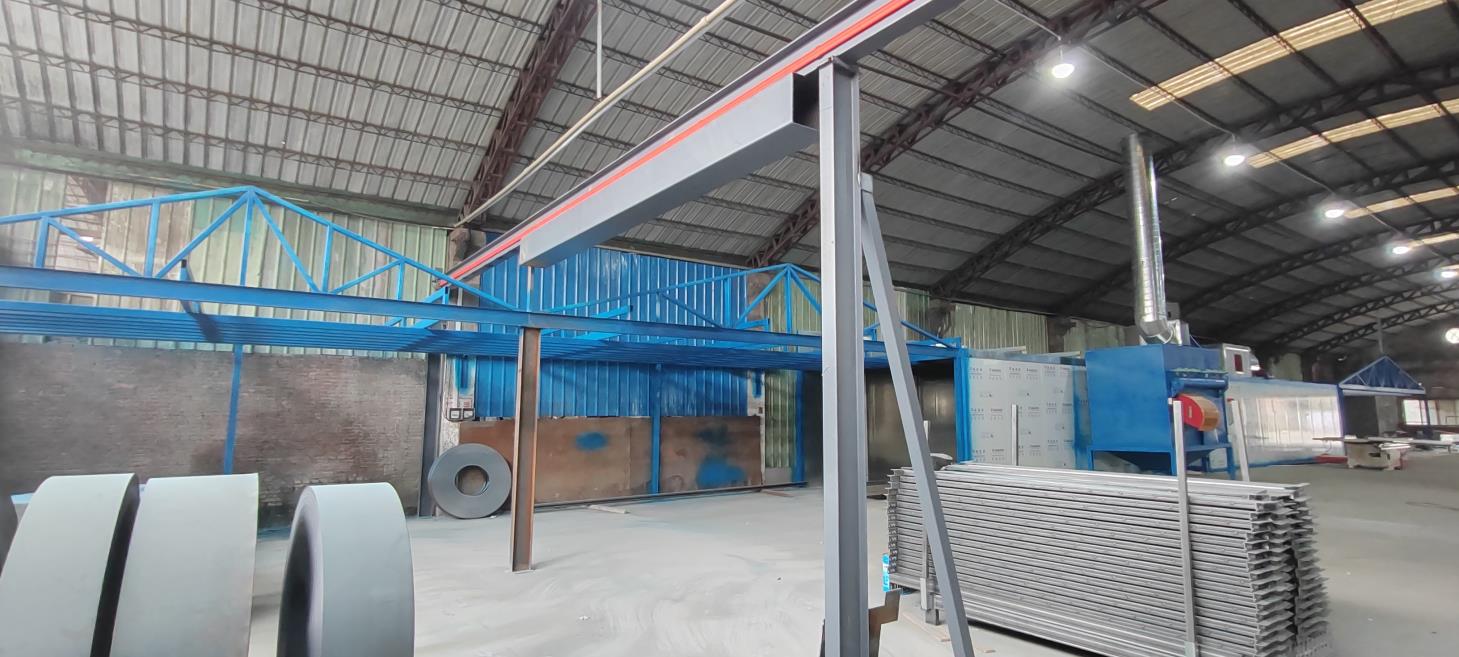
Established in 2016, Nanjing Fortis Storage Equipment Manufacturing Co., Ltd. commands a modern industrial plant covering 48,000 m². Driven by 10 years of deep industry expertise and 7 years of global trade experience, our annual export turnover reaches $35 million. We uphold strict quality control through ISO14001 and TUV standards, performing automated CMM dimensional inspections and salt spray corrosion testing with 62 full-time QA personnel. As a direct factory exporter, our key commercial footprints span Western Europe, South America, and the Middle East, integrated with a network of over 1,400 supply chain partners. Our client base mainly includes mega-warehouse developers, cold chain storage operators, and global retail chains. Our robust R&D team of 80 engineers specializes in bespoke structural adaptations, special surface coating treatments, and high-density racking configurations, introducing 350 innovative products to the global market last year.
As supply chain paradigms rapidly evolve toward hyper-automation, storage containers and industrial racking systems are no longer static structural components. They have transformed into dynamic nodes within interconnected IoT ecosystems. Our strategic technology roadmap focuses on the integration of smart-embedded sensors, high-strength lightweight alloy matrices, and sustainable circular-economy manufacturing techniques.
Looking toward the future, automated storage and retrieval systems (AS/RS) require exceptionally tight tolerances and optimized weight-to-load ratios. By incorporating advanced finite element analysis (FEA) during our engineering design phase, we simulate extreme structural stress scenarios, seismic shifts, and cyclical fatigue loadings. This ensures our storage containers deliver unparalleled longevity and safety compliance across diverse global operational environments.
Global enterprises, ranging from e-commerce logistics giants to multi-national retail conglomerates, encounter distinct operational bottlenecks. Mega-warehouse developers demand ultra-high-density storage solutions to maximize cubic capacity utilization, whereas cold chain storage operators require corrosion-resistant, cryogenic-stable materials that withstand sub-zero temperatures without compromising structural integrity.
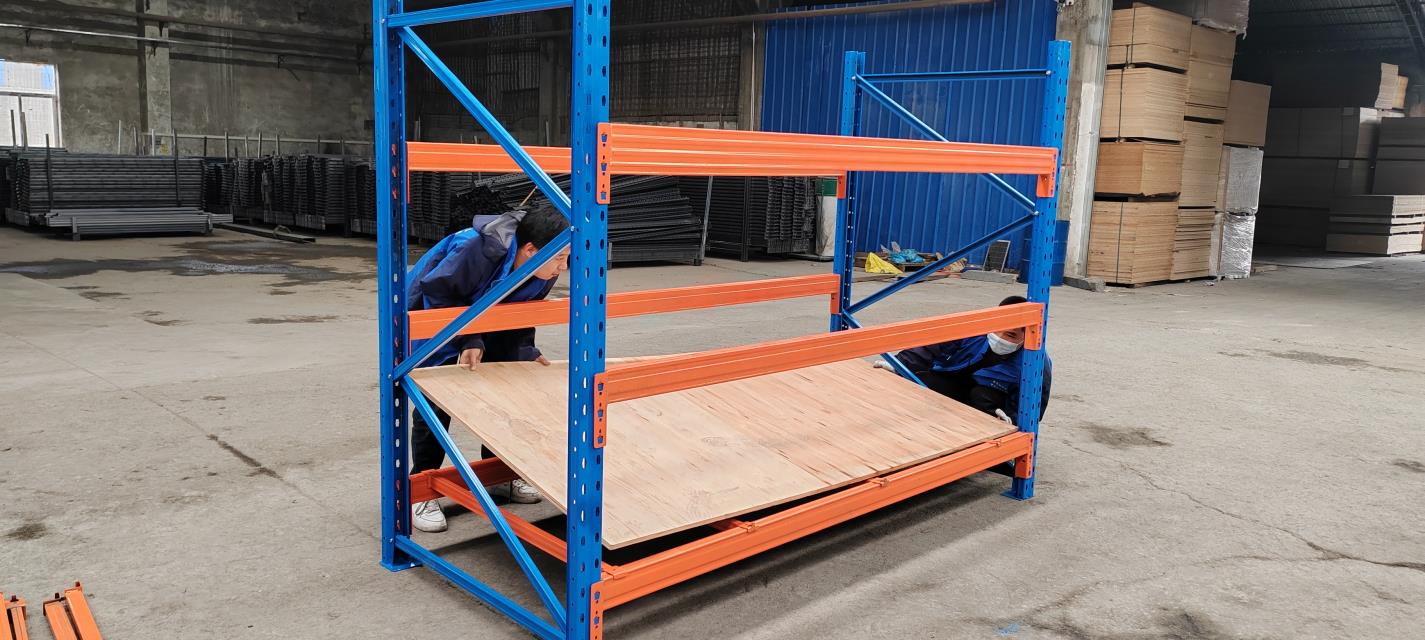
Our macro industry solutions bridge these complex challenges through modular configurability and heavy-duty load capacities. By understanding regional zoning laws, seismic load requirements, and specific SKU rotation frequencies, our engineering consultants formulate bespoke architecture that minimizes throughput friction and optimizes inventory turnover ratios for international buyers.
Navigating international regulatory frameworks is critical for seamless cross-border procurement. We maintain rigorous adherence to globally recognized certifications, including ISO14001 environmental management protocols and stringent TUV safety validations. Every batch of storage containers and structural steel undergoes rigorous automated CMM dimensional inspections and salt spray corrosion testing.
Our dedicated regulatory compliance team works closely with overseas clients to ensure all export shipments satisfy destination-specific building codes, fire safety mandates, and occupational health standards. This meticulous attention to detail mitigates customs clearance delays and guarantees risk-free operational deployment from day one.
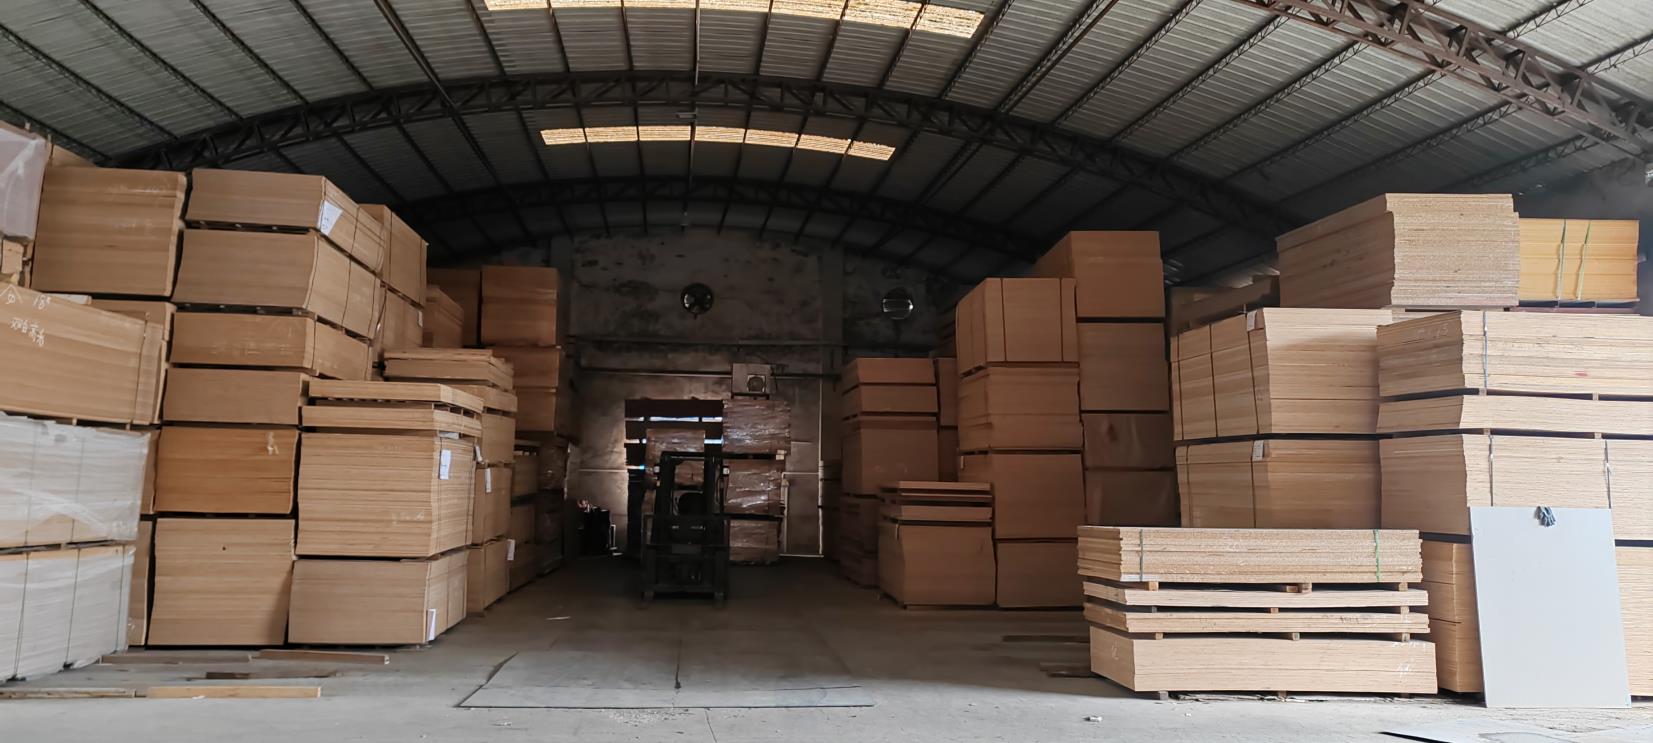
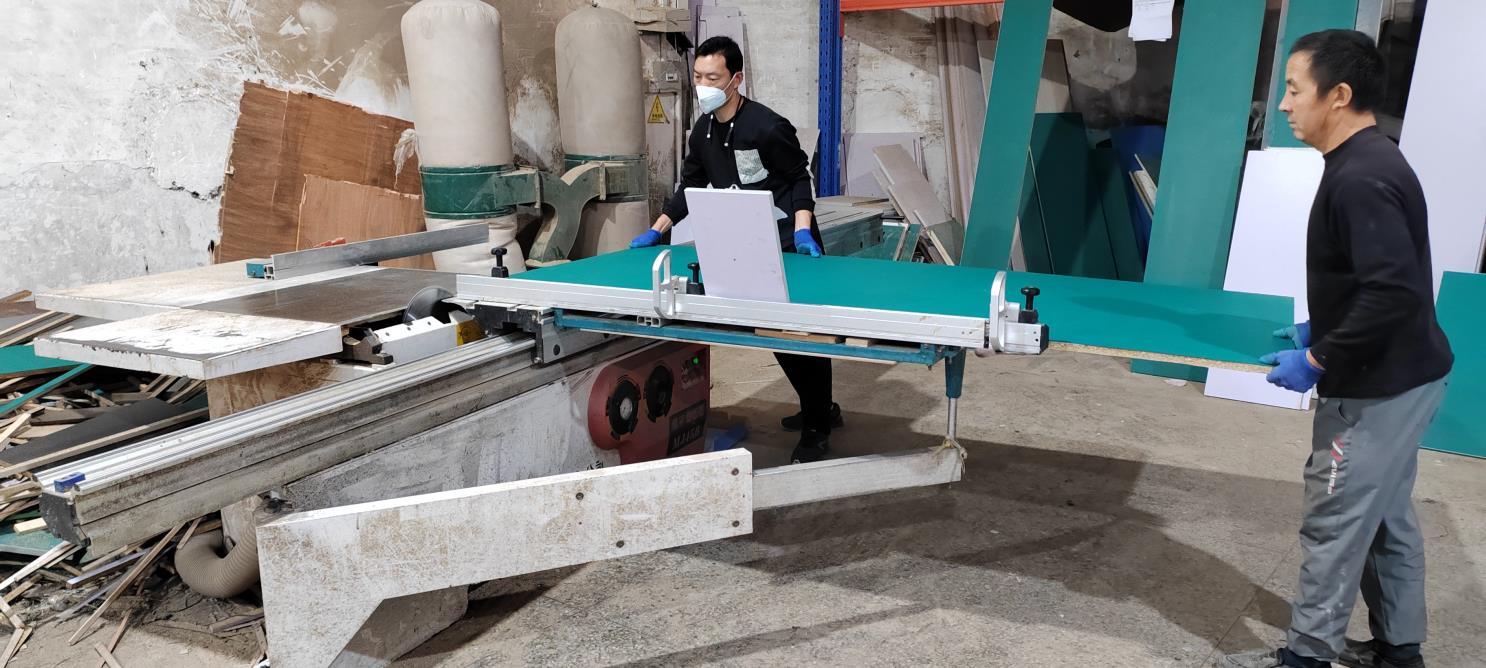
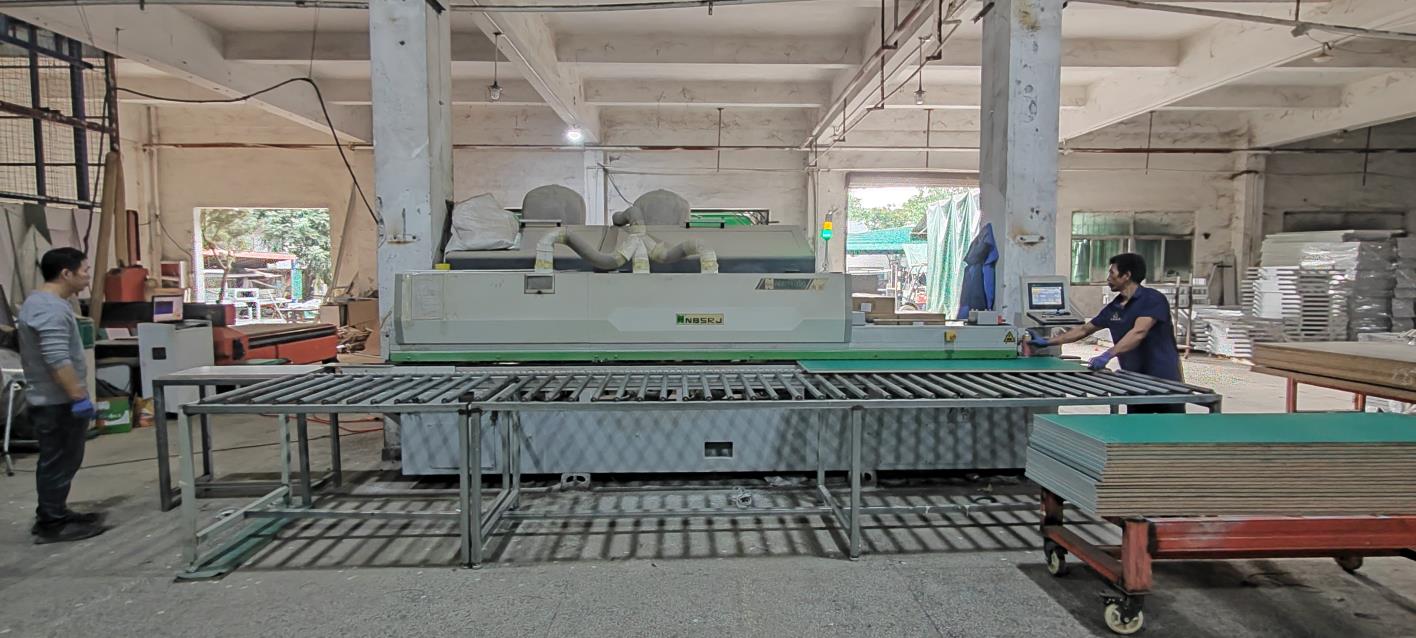
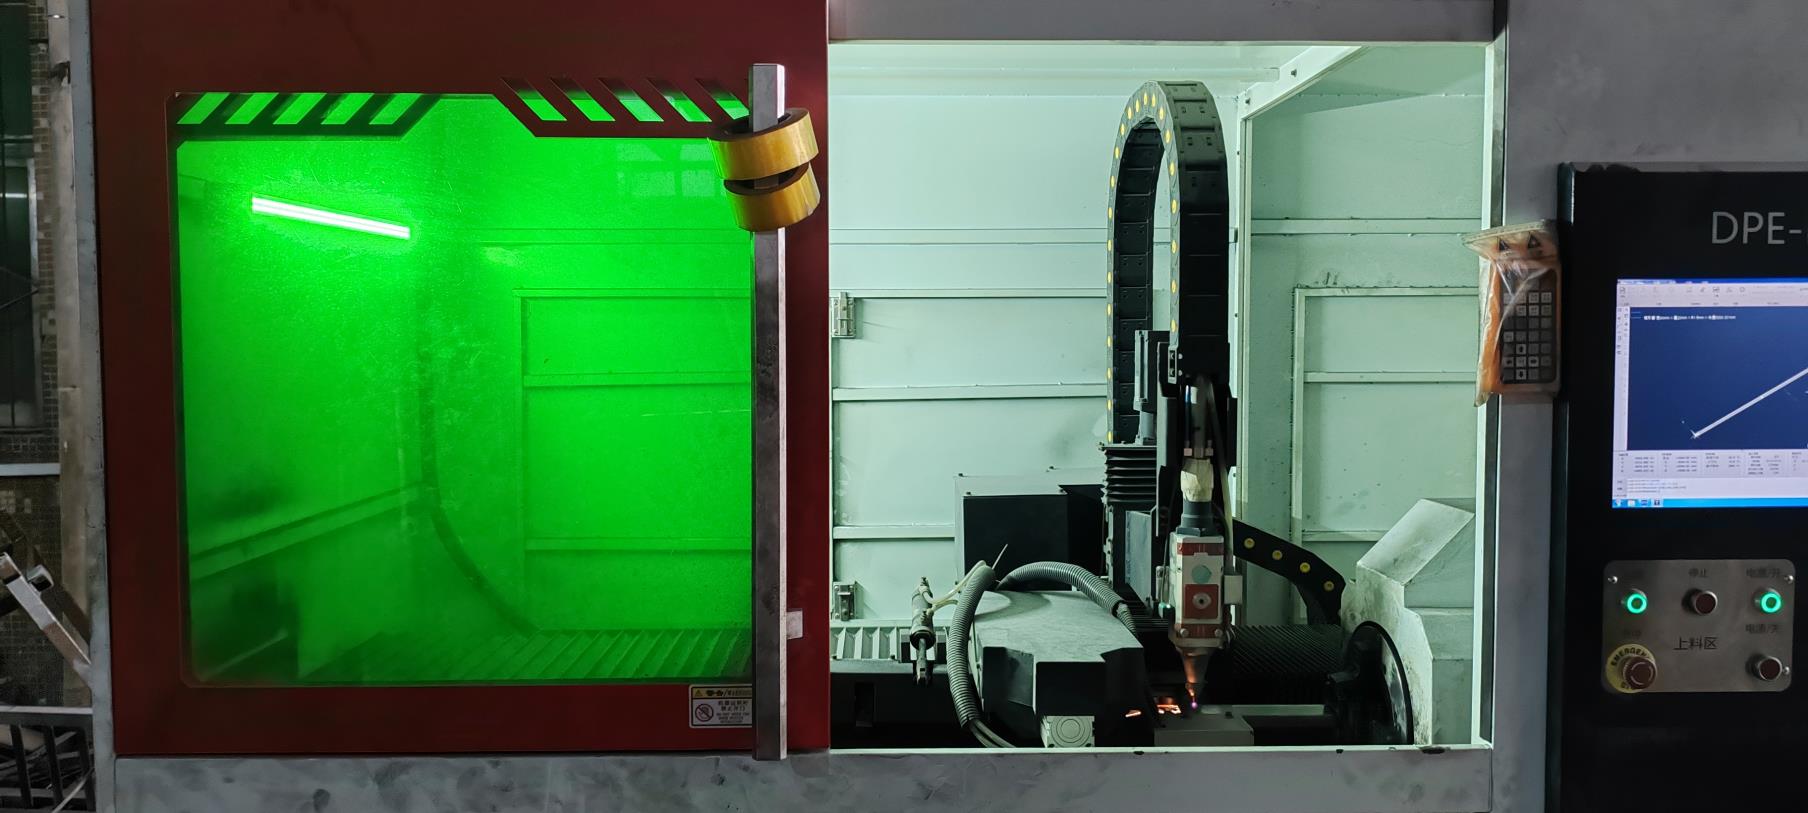
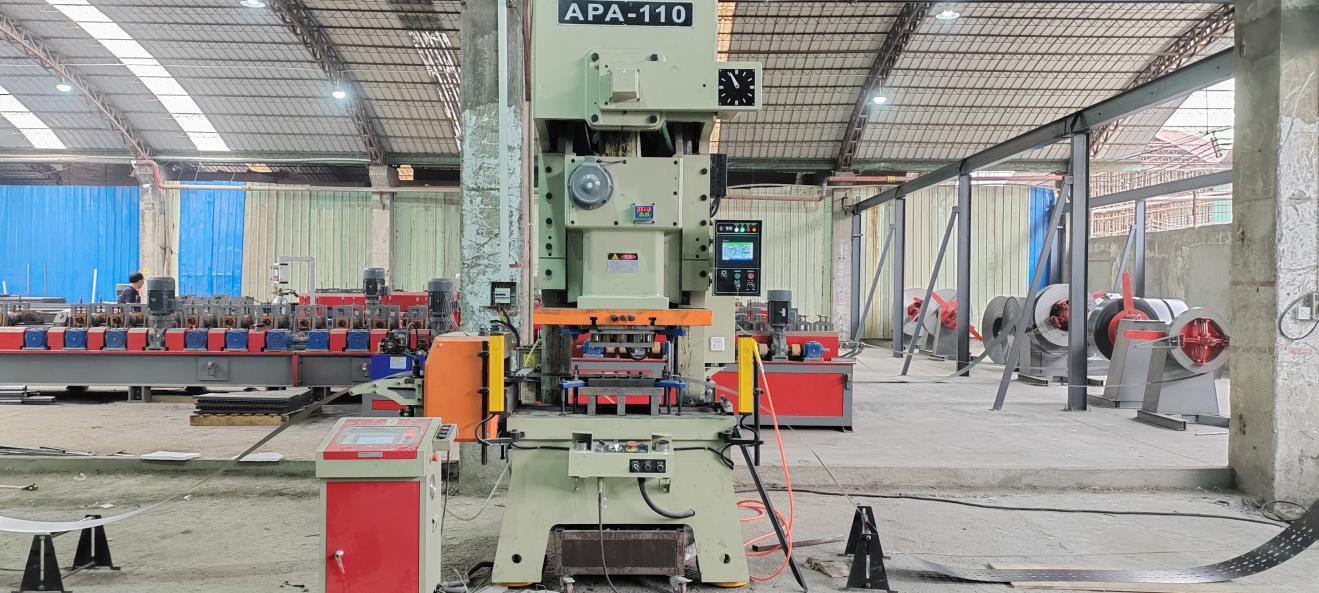
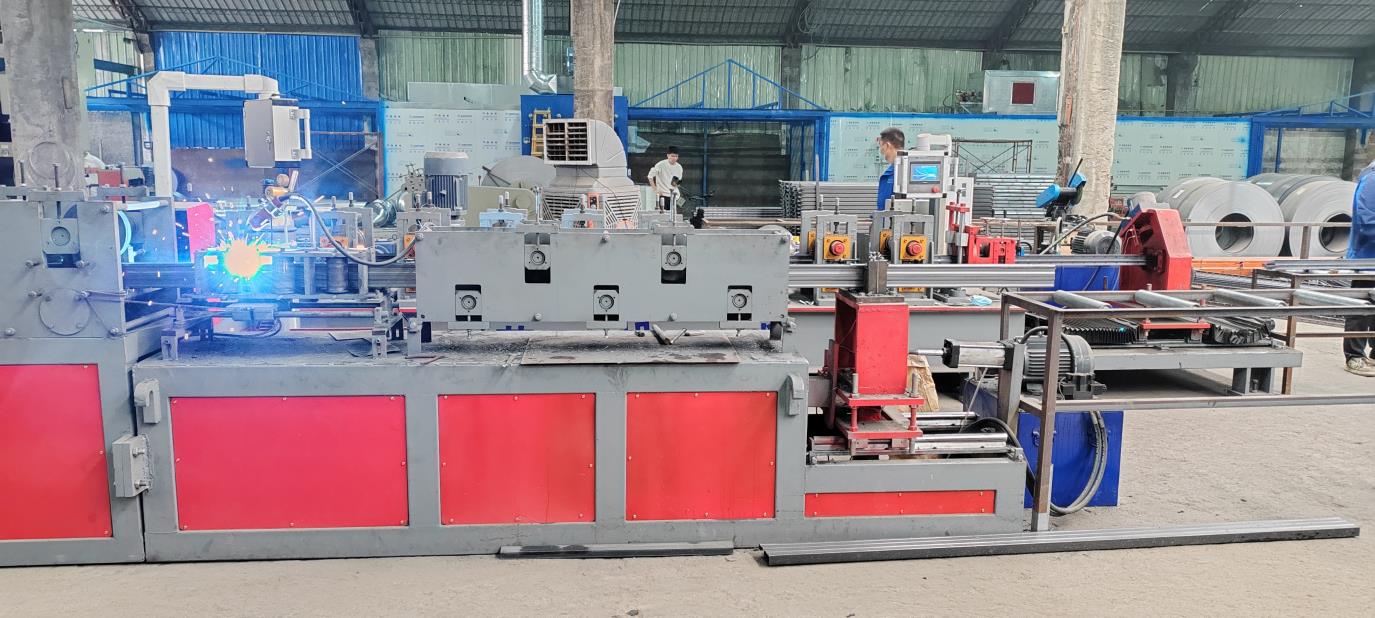
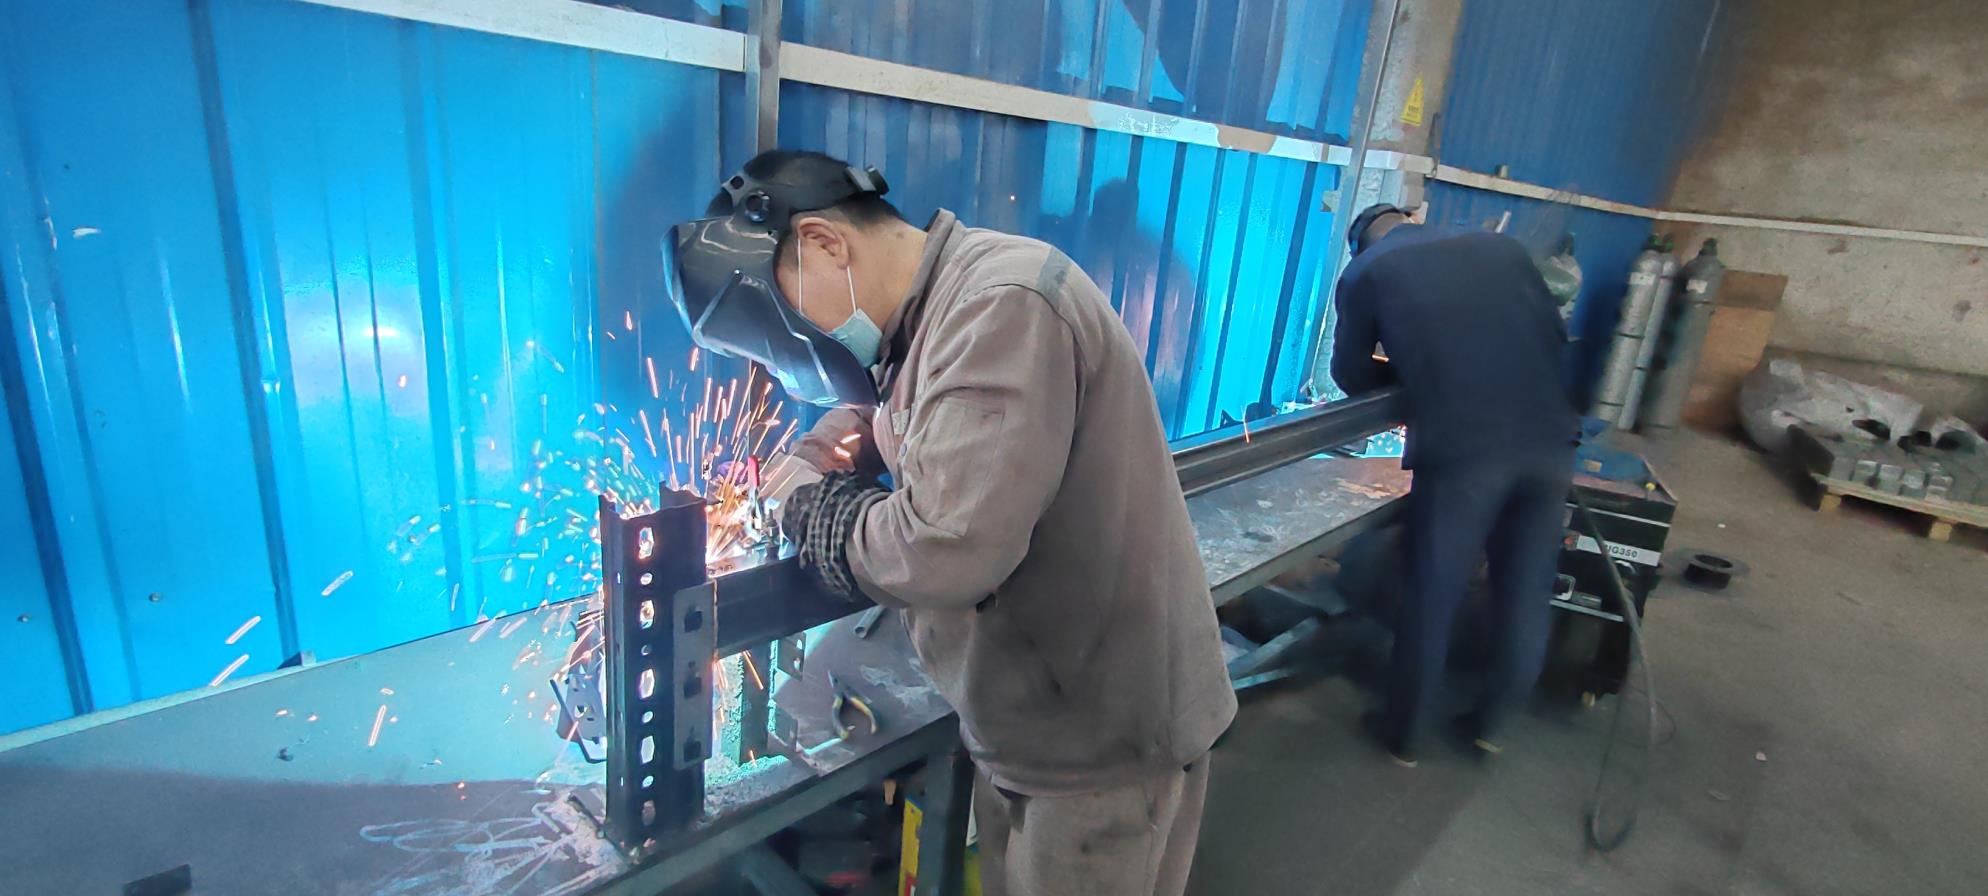
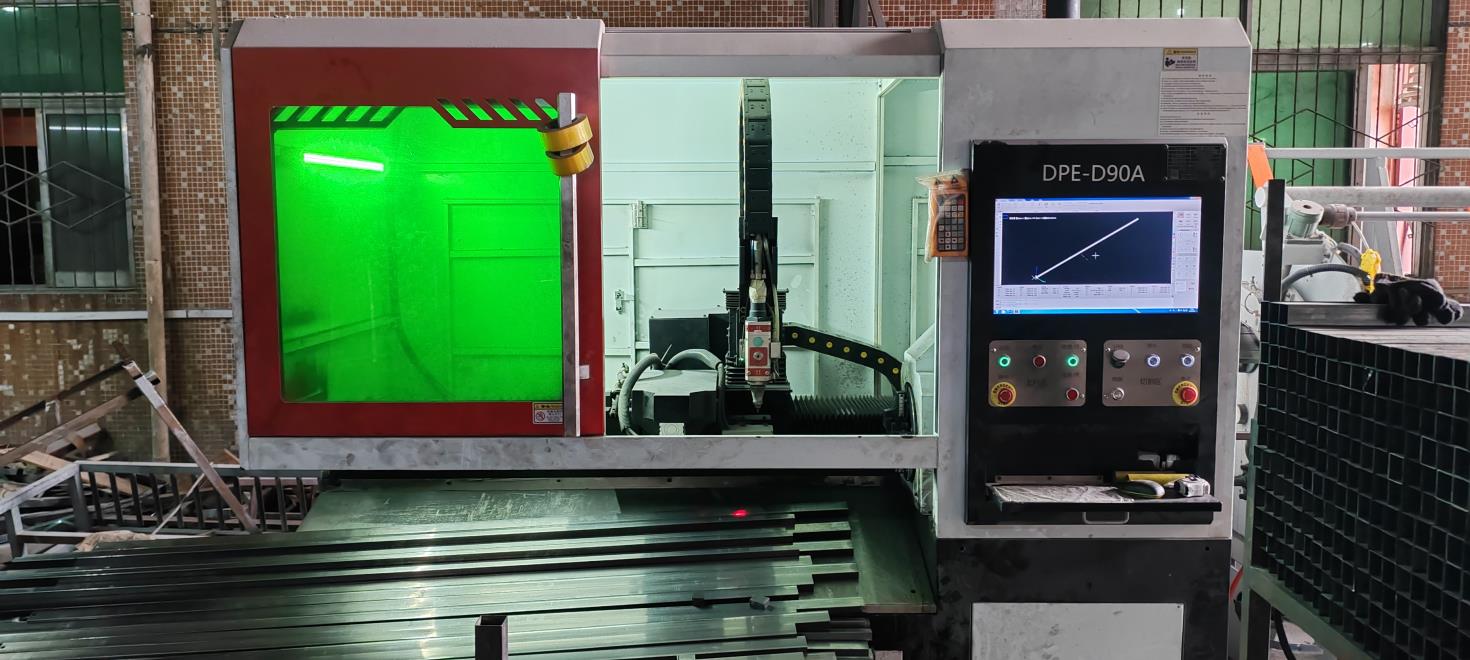
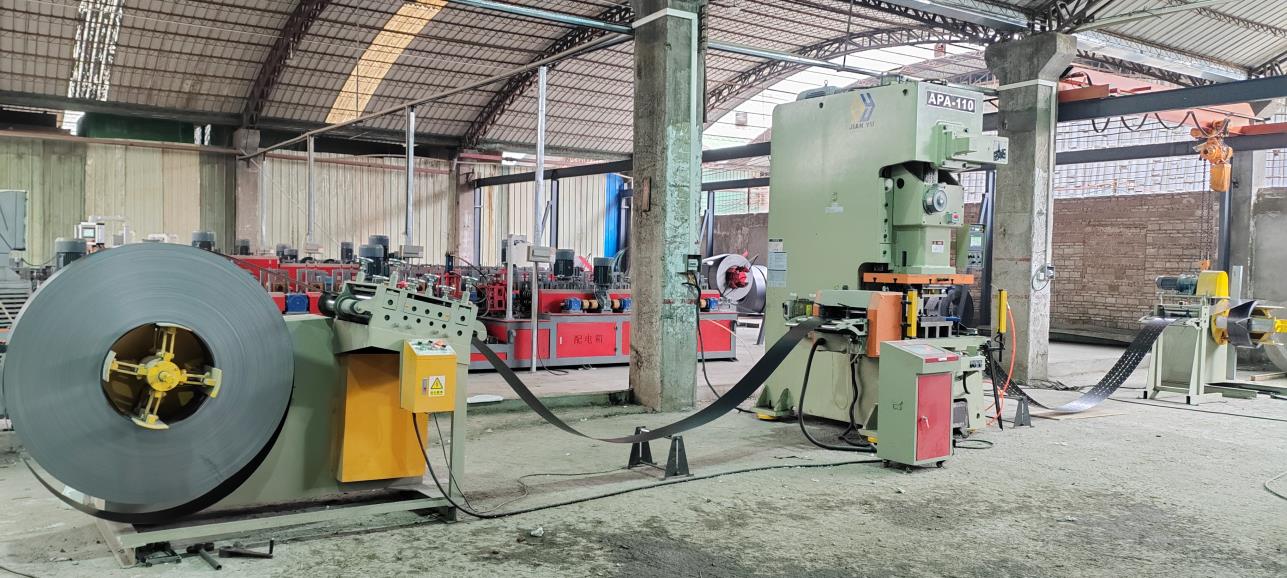
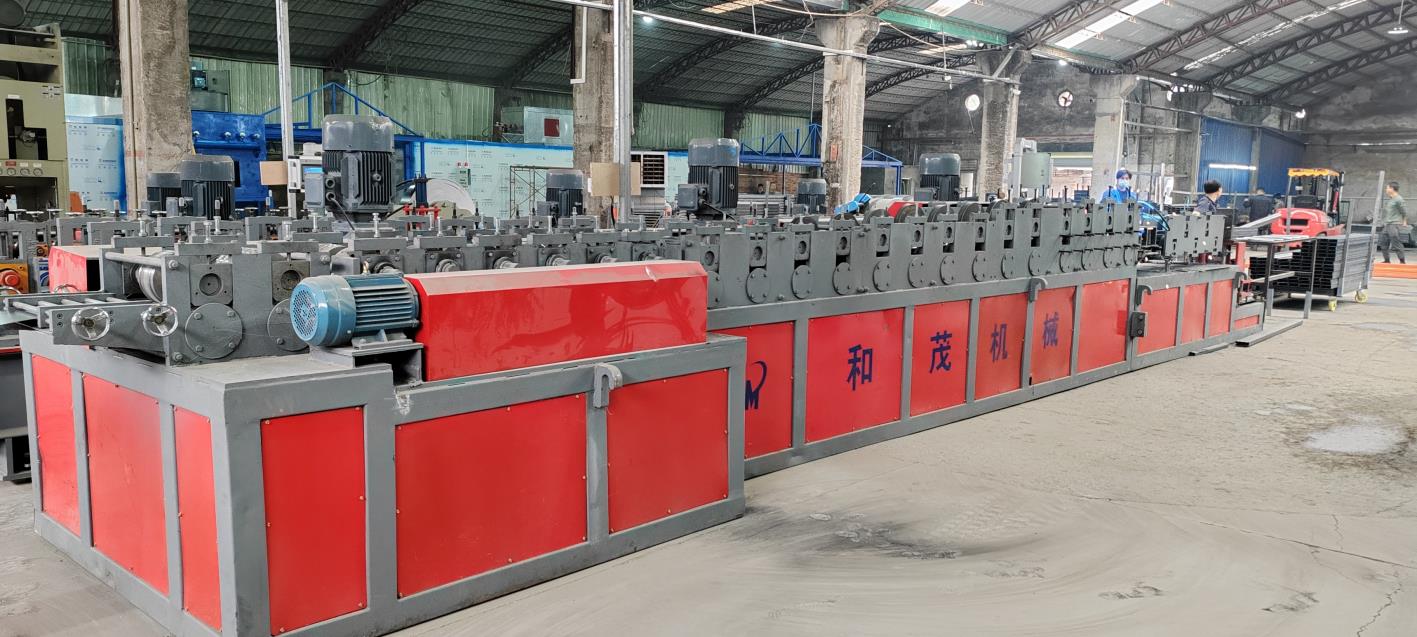
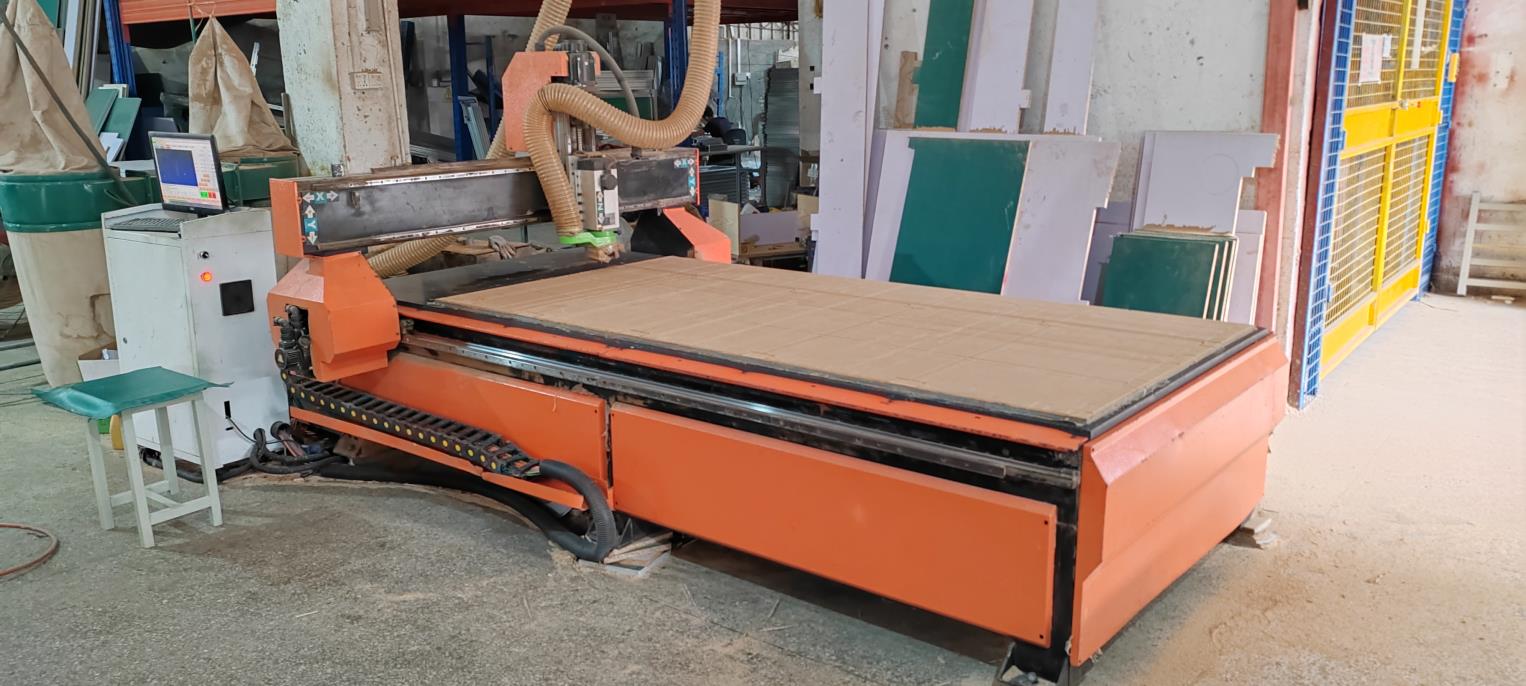
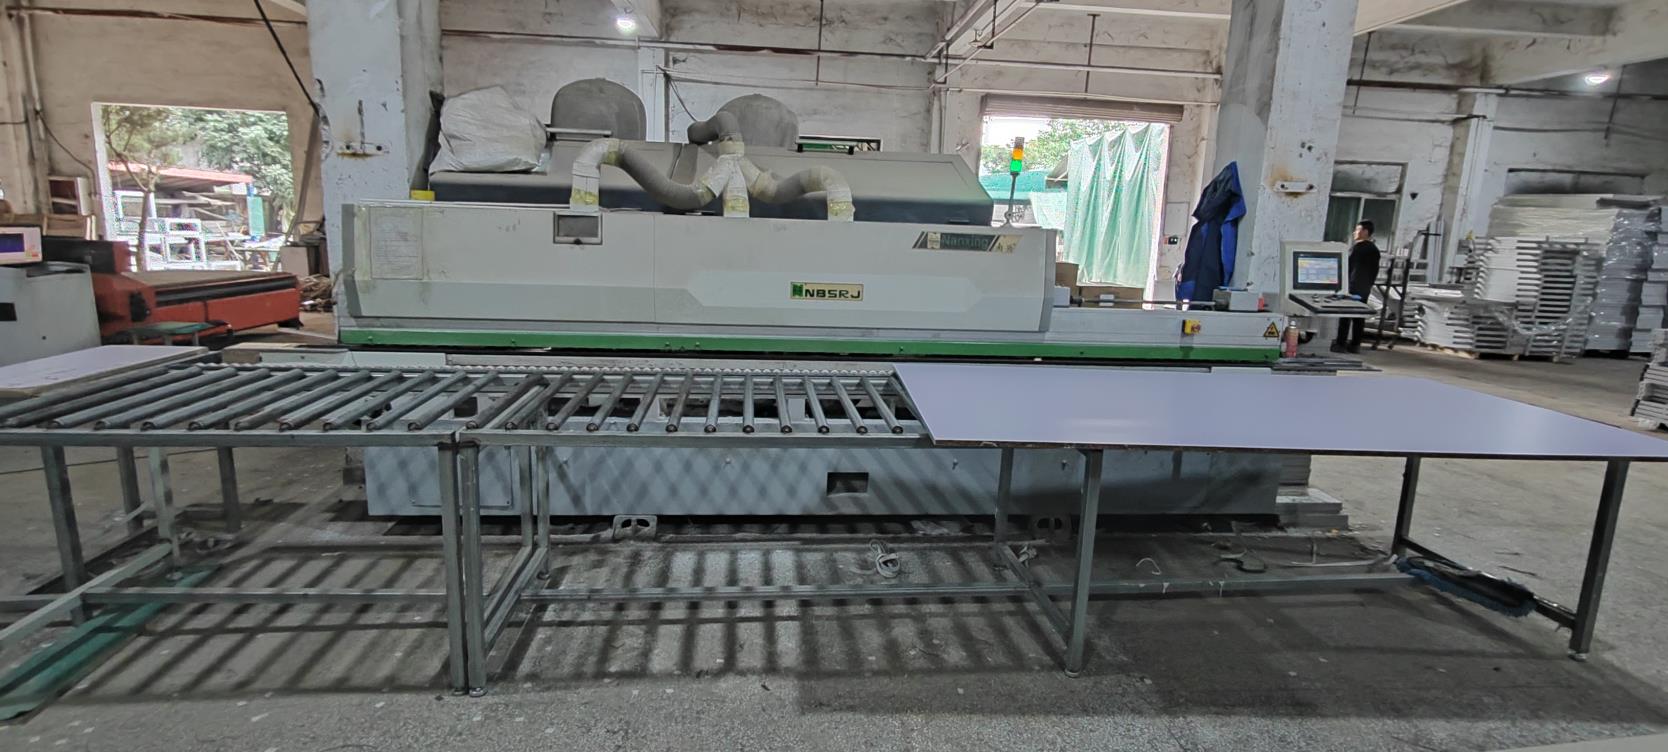
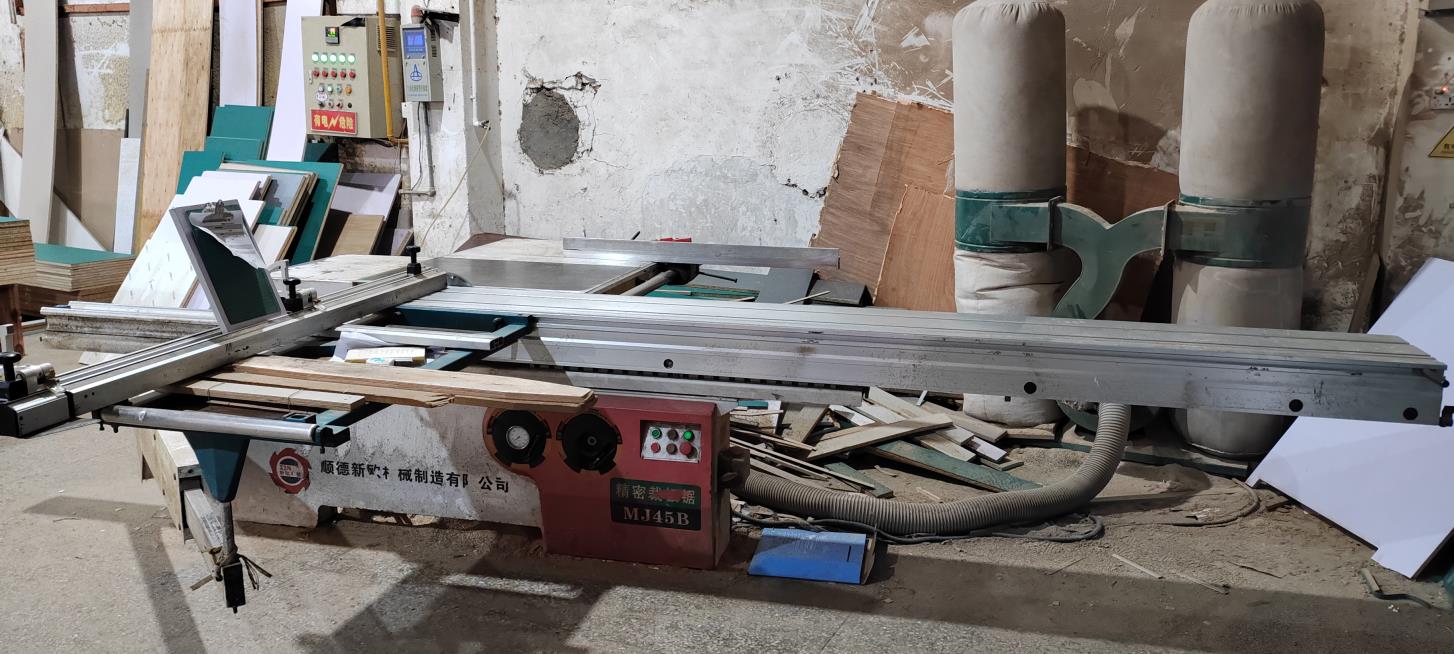
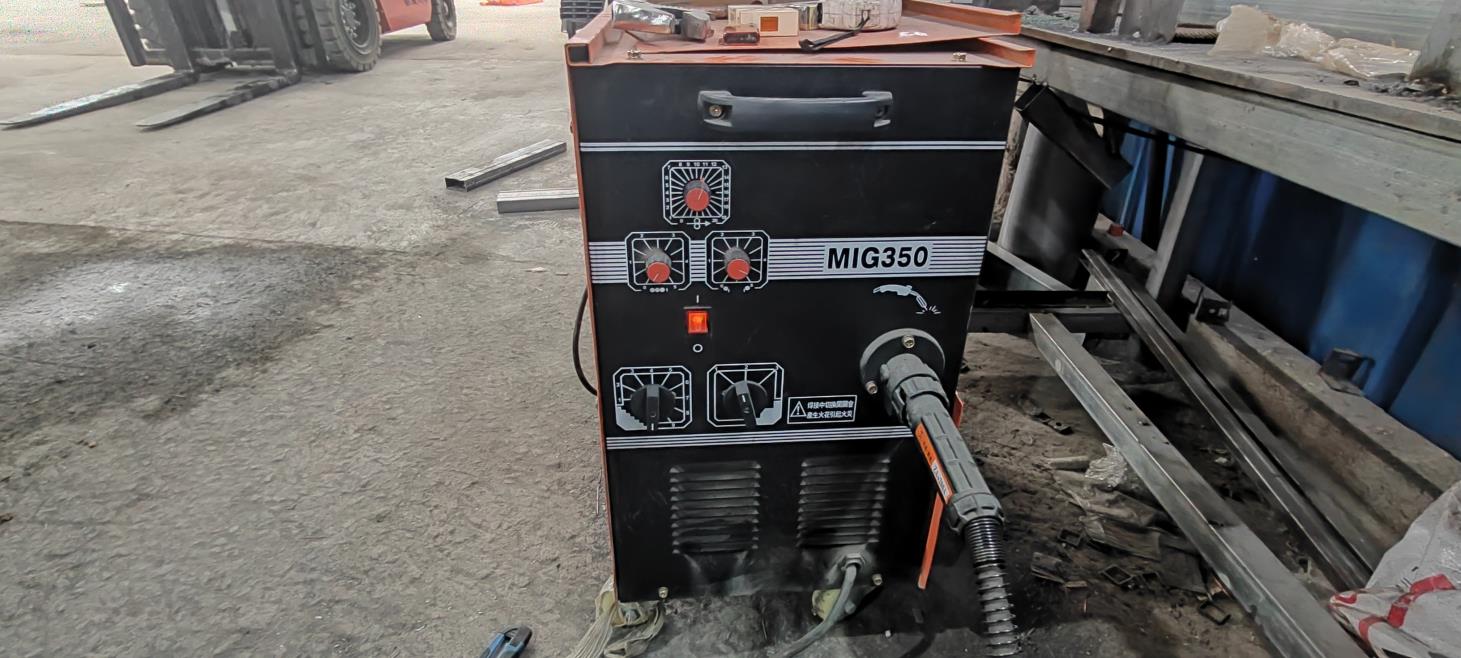
Representing the forefront of China Factory 4.0 paradigms, our 48,000 m² manufacturing facility integrates advanced automation, robotic welding arrays, and computerized laser cutting centers. This high degree of technological integration guarantees exceptional repeatability, zero-defect production runs, and accelerated lead times.
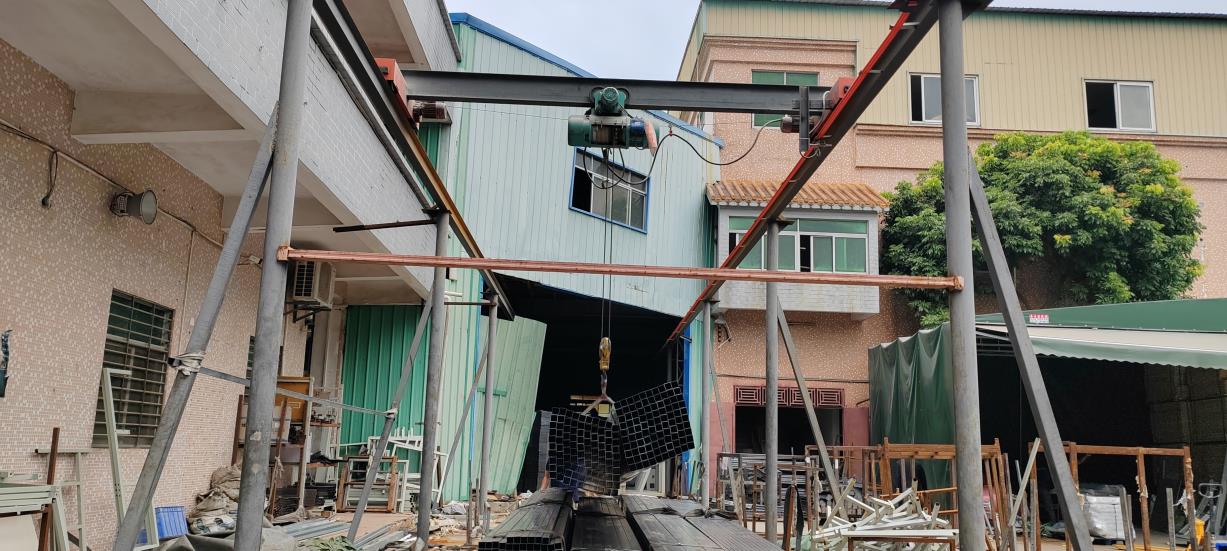
Our resilient supply chain ecosystem, anchored by over 1,400 vetted partner tiers, insulates our operations from raw material volatility. By utilizing centralized procurement strategies and intelligent inventory forecasting, we ensure continuous production flow and predictable, competitive cost structures for our global B2B clientele.
Q1: What are your minimum order quantities (MOQ) for OEM/ODM storage containers?
A1: As a direct manufacturer with a 48,000 m² factory, we offer flexible MOQ terms tailored to specific project scales, supporting both pilot orders and full-scale commercial rollouts.
Q2: How do you ensure product quality and corrosion resistance for export markets?
A2: We employ 62 full-time QA personnel executing automated CMM dimensional checks, strict TUV standards, and salt spray corrosion testing on all surface coatings.
Q3: Can your engineering team customize racking dimensions for specific warehouse layouts?
A3: Yes. Our 80 specialized R&D engineers excel in bespoke structural adaptations, high-density configurations, and specialized load-bearing optimizations.
 FortisRack